

Pneumatic actuators on industrial valves usually fail prematurely for one of six reasons: low or unstable air pressure, air leakage, contaminated or restricted air paths, control-accessory faults, mechanical wear or misalignment, and an actuator that cannot meet the valve’s torque or thrust demand. These faults can produce similar symptoms, so a slow or immobile valve does not by itself prove that the actuator has failed.
A sound diagnosis separates the command signal, instrument-air system, solenoid or positioner, actuator, mounting parts and valve load. The most useful checks are the real command and feedback, pressure at the actuator inlet while the valve moves, the leakage and exhaust path, mechanical freedom, and actuator output compared with valve demand under the same operating conditions.
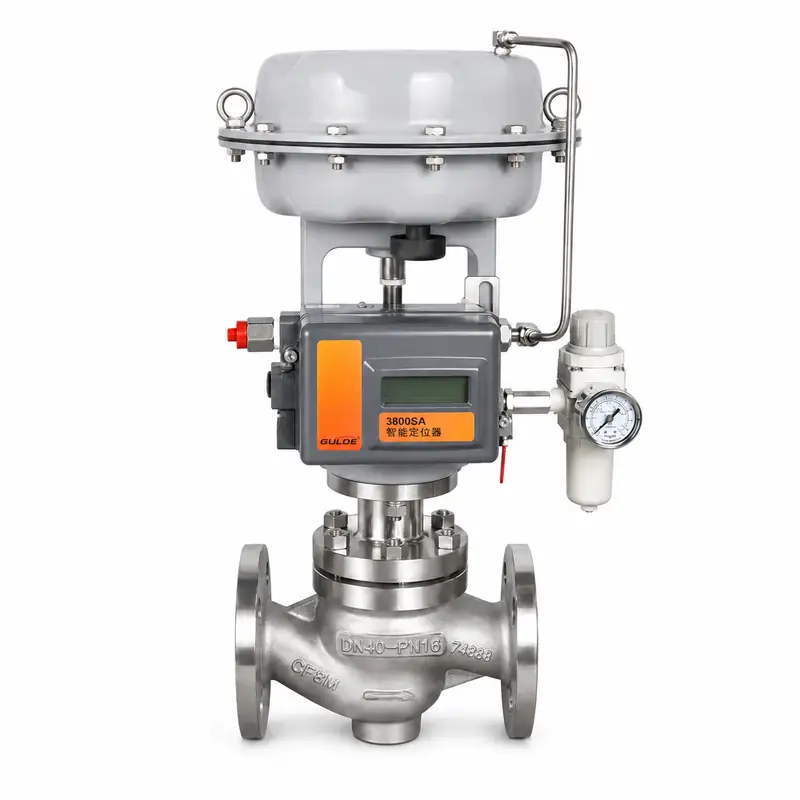
What causes pneumatic actuators to fail prematurely?
Early failure often starts outside the actuator housing. A weak supply, blocked exhaust, faulty solenoid or hard-to-move valve can make a healthy actuator look defective. Check each fault area before replacing seals or the complete unit.
Low or unstable air supply
A pressure gauge can show a normal reading while the valve is idle, then fall as soon as the actuator starts to move. This dynamic pressure loss may come from a small supply tube, partly closed isolation valve, blocked filter, poor regulator setting, long air line or limited header capacity. The result may be slow travel, low output, failure near the end of stroke or a fault that appears only when other air users are active.
Measure pressure at the actuator inlet during both opening and closing. Compare it with the regulator outlet and supply header at the same time. Inspect the bowl, drain and filter element of the air filter regulator if the pressure drop is too high. Do not raise the setting above the rating of the actuator, solenoid, positioner or tubing.

Air leaks and worn seals
External leakage at a fitting, tube or housing joint reduces the pressure available for motion. Continuous flow from an exhaust port needs more care because the leak may be inside the solenoid or positioner, across the actuator piston seals, or through a damaged diaphragm. Localise the leak with an approved method while the equipment is in a safe test state. Replacing actuator seals will not correct leakage that starts in an accessory.
The leak path also changes with the actuator design. A spring-return actuator has one powered direction and stored spring energy, while a double-acting actuator uses air for both directions. The checks in the single-acting and double-acting actuator comparison help identify which ports and chambers should be pressurised in each state.
Contaminated air and restricted exhaust
Water, oil carry-over, rust and loose particles can damage seals, score moving surfaces or block small pilot passages. A clogged exhaust silencer, kinked tube or blocked vent can hold back the returning air and make one direction much slower than the other. This pattern is often mistaken for a weak actuator.
Drain collected water, check the filter element, inspect vents and silencers, and confirm that exhaust air has a clear path. Use the air quality and lubrication stated by the actuator and accessory manufacturers. Adding line lubricant where it is not specified can affect seals or collect more dirt.
Solenoid, positioner, tubing or feedback faults
A valid command on the control screen does not prove that the actuator received the correct pressure. Check the signal at the field device, solenoid coil voltage and connector condition, pilot pressure, positioner supply and output, tube routing, and the actual valve position. A loose feedback arm or poorly set limit switch can report an open or closed state that the valve has not reached.
When several accessories are fitted, trace the signal and air path in order instead of changing several settings at once. The guide to pneumatic valve accessories explains the separate jobs of solenoid valves, positioners, limit switches and air preparation parts.
Mechanical wear, corrosion or misalignment
Loose brackets, coupling wear, shaft or stem misalignment, side load, corrosion and excess backlash can absorb actuator movement or increase friction. ISO 5211 mounting dimensions help match a quarter-turn actuator to a valve interface, but the standard interface alone does not prove that the assembled shafts are aligned or that the coupling length is correct. Check the bracket, fasteners, coupling engagement and travel stops as one drive train. The ISO 5211 mounting guide shows the interface details that must be confirmed.
Inspect these parts only after the valve package has been made safe. Do not uncouple a spring-return actuator or force a process valve by hand until the approved procedure has dealt with process pressure, stored spring energy and possible valve movement.
Incorrect sizing or excessive valve load
An actuator may stroke normally on a bench but stop when it is connected to the valve. Compare actuator output with valve demand at the same minimum dynamic air pressure, temperature, travel position and fail direction. The comparison must cover the load that actually governs the application:
- Quarter-turn valves: break, running and end-of-travel torque under the real differential pressure and flow direction.
- Linear valves: stem thrust needed to move the plug, overcome packing friction and meet the shut-off requirement.
- Changing service: deposits, temperature, seat condition, packing adjustment and long idle periods that can raise the load after commissioning.
There is no safe universal service factor for every valve and duty. Use the valve maker’s torque or thrust data and the actuator maker’s output data, with the project conditions and required fail action. The pneumatic actuator sizing guide covers this comparison. Oversizing is not a complete cure because excess output can damage stems, shafts, seats, stops or mounting parts.
Match the symptom to the likely fault area
Use the symptom to choose the first test, not to name the failed part. Direction, load, process state and whether the fault is constant or intermittent all change the likely branch.
| Observed symptom | Likely fault area | First check |
|---|---|---|
| No movement | Command, solenoid, air supply or seized drive | Confirm the field command and inlet pressure |
| Slow or weak travel | Dynamic pressure loss, leak, restricted flow or high valve resistance | Compare idle and moving pressure in both directions |
| Stops short at a repeatable point | Output shortfall, travel-stop error, misalignment or rising valve load | Record pressure and actual position at the stop point |
| Erratic or hunting motion | Positioner, contamination, friction, loose linkage or feedback error | Compare command, positioner output and real travel |
| Continuous air leakage | Fittings, solenoid, positioner, piston seals or diaphragm | Find whether the leak is external or from an exhaust port |
| Indicated position differs from the valve | Feedback linkage, switch setting, calibration or coupling slip | Verify the valve position at the shaft or stem |
More than one branch may be active. For example, low moving pressure can combine with a stiff valve and make a marginal actuator fail only at peak process load. Broader valve-side fault paths are grouped in the valve troubleshooting and maintenance resource hub.
Troubleshoot the valve package in a fixed sequence
Move from shared inputs towards internal actuator faults. This keeps a blocked filter, lost command or stiff valve from being hidden by an early seal replacement. Stop the test if the valve moves without control, process containment is in doubt, or the work needs dismantling beyond the approved maintenance scope.
Tests must start with the site’s procedure for process pressure, pneumatic pressure, electrical power and stored spring energy. Where it applies, OSHA 29 CFR 1910.147 sets requirements for the control of hazardous energy. The official lockout/tagout rule is a safety reference, not a substitute for the site’s procedure.
- Make the valve package safe. Isolate every energy source, deal with stored energy as required, and verify the safe state before testing.
- Define the fault before changing anything. Record the direction, travel point, stroke time, process condition, air pressure, command and feedback. Note whether the fault is constant, load-related or intermittent.
- Verify command and actual position. Check the electrical or pneumatic command at the field device. Compare indicated travel with the real shaft or stem position so a feedback fault is not mistaken for failed motion.
- Measure air pressure while the actuator moves. Test at the actuator inlet in both directions and watch for pressure loss through the regulator, filter, valve, fittings or tubing. An idle gauge reading is not enough.
- Inspect the supply, leak and exhaust paths. Check tubing, fittings, drains, filter elements, silencers and vents. Find whether continuous leakage is external, from a control accessory or from the actuator before opening any housing.
- Check solenoid or positioner output. Confirm that the command pressurises the correct port and lets the other side exhaust. Keep every test within the site’s safe method and the device rating.
- Inspect the mechanical drive. Check brackets, fasteners, couplings, shafts or stems, travel stops, backlash, corrosion and signs of rubbing. Test valve freedom only when isolation and the approved procedure allow it.
- Compare output with valve demand. Use the measured minimum pressure and the makers’ output and torque or thrust data for the real process condition and fail direction.
Keep the readings taken before and after the correction. If several settings or parts are changed together, the team loses the evidence needed to prevent the same failure from returning.
Maintenance checks that prevent repeat failures
A fixed calendar does not reflect every actuator’s cycle rate, load or environment. Start with the maker’s instructions and site rules, then trend a small set of readings under similar operating conditions. A change from the unit’s own baseline is often more useful than a general limit taken from another valve.
| Check | Change to watch | Follow-up |
|---|---|---|
| Stroke time in each direction | Longer travel or a growing difference between directions | Check dynamic pressure, exhaust and valve resistance |
| Air leakage or air use | New hiss, continuous exhaust or rising consumption | Find the leak path before replacing seals |
| Air preparation | Water, dirt, oil carry-over or pressure drift | Drain, clean or service the specified component |
| Command and travel agreement | More position error, hunting or failed end indication | Inspect the positioner, switches, linkage and calibration |
| Mounting and drive parts | Loose fasteners, backlash, rubbing or corrosion | Correct alignment and replace confirmed worn parts |
| Output against valve load | Less margin after a process, packing or seat change | Repeat the torque or thrust comparison |
There is no single service life for a pneumatic actuator. Life changes with cycle count, valve load, air quality, temperature, corrosion, vibration, seal material, spring duty and how often the valve stays still. Record stroke time, leakage and travel error from commissioning onward, then shorten the inspection interval when the trend changes or the service becomes more severe.
Conclusion
Premature pneumatic actuator failure is confirmed only after the command, moving air pressure, accessory output, mechanical drive and valve load have been separated. If testing confirms an internal actuator fault or an output shortfall, compare the required motion, fail action and torque or thrust with the available pneumatic actuator options for industrial valves before repair or replacement.