

A control valve is not ready for start-up when the flange bolts are tight. The installed package must also be clean, correctly aligned and supported, supplied with the specified instrument air or electrical power, and connected to the correct control and feedback signals. A directional valve fitted against its marked flow arrow, loaded by misaligned pipework, or exposed to weld slag during flushing may pass a visual check but fail when it is asked to move.
Commissioning must prove the whole operating chain. This includes checking positioner zero, span and full travel against the valve and actuator documents, then testing the defined fail action, solenoid valve, limit switches and interlocks under the correct loss-of-air, loss-of-power or loss-of-signal condition. Once process fluid is introduced, the first stable operating data should be recorded as a baseline for later fault finding. Exact pressure settings, travel limits, stroke times and acceptance values must come from the approved datasheet, P&ID, loop drawings, cause-and-effect matrix and manufacturer instructions for that valve package.
Control foreign material before the valve sees the line
Line cleaning can damage a new control valve before commissioning begins. Weld slag, pipe scale, sand, sealant and loose metal may cut seating surfaces, lodge between the plug and seat, or block small trim passages. The approved cleaning method must prevent this material from reaching the valve internals before the piping-cleanliness requirement has been met.
Flush or blow the piping without sacrificing the trim
Use the approved piping cleaning procedure together with the valve manufacturer’s installation and maintenance instructions. Depending on the valve design and project method, the valve may be replaced by a temporary spool, removed, isolated from the cleaning flow, or held in a defined position during flushing or blowing. The cleaning medium, direction, flow rate and acceptance limit are service-specific. A method suitable for metal trim may damage a soft seat or leave unflushed pockets in another valve design.
If a temporary screen or strainer is required, confirm that its mesh, pressure-drop limit and location suit the cleaning duty. Its installation and removal should be recorded. A forgotten temporary screen may restrict flow after start-up, while a damaged screen may release the debris it was meant to retain.
Keep debris out after cleaning and before start-up
A cleaned line can be contaminated again while flanges, vents or instrument connections remain open. Keep protective covers and caps in place until each connection is ready for assembly. Before final bolt-up, inspect the valve bore, gasket faces and nearby pipe ends, then remove loose scale, weld spatter, tape and excess joint compound. Gaskets must remain centred and must not project into the flow path.
Before commissioning, confirm the final state of temporary blinds, flushing connections, screens, strainers and protective covers against the approved start-up procedure. Record the piping-cleanliness acceptance and final inspection so there is clear evidence of when the valve trim was first exposed to the process line.
Install the valve and actuator without adding mechanical error
Flow direction must be established from the valve body markings and approved piping documents. A flow arrow shows the direction for which a directional valve was selected or built, while port markings identify the correct connections on multi-port designs. Installing the assembly against these markings may change its capacity, stability, shut-off load or noise behaviour.
Follow body arrows, port markings and the approved flow path
Before lifting the valve into place, match its tag and nameplate to the datasheet, piping and instrumentation diagram, installation drawing and line designation. The process flow shown on those documents must agree with the body arrow or port layout. Do not infer flow direction from actuator movement or the Fail Open or Fail Close description because fail action and permitted process flow are separate design choices.
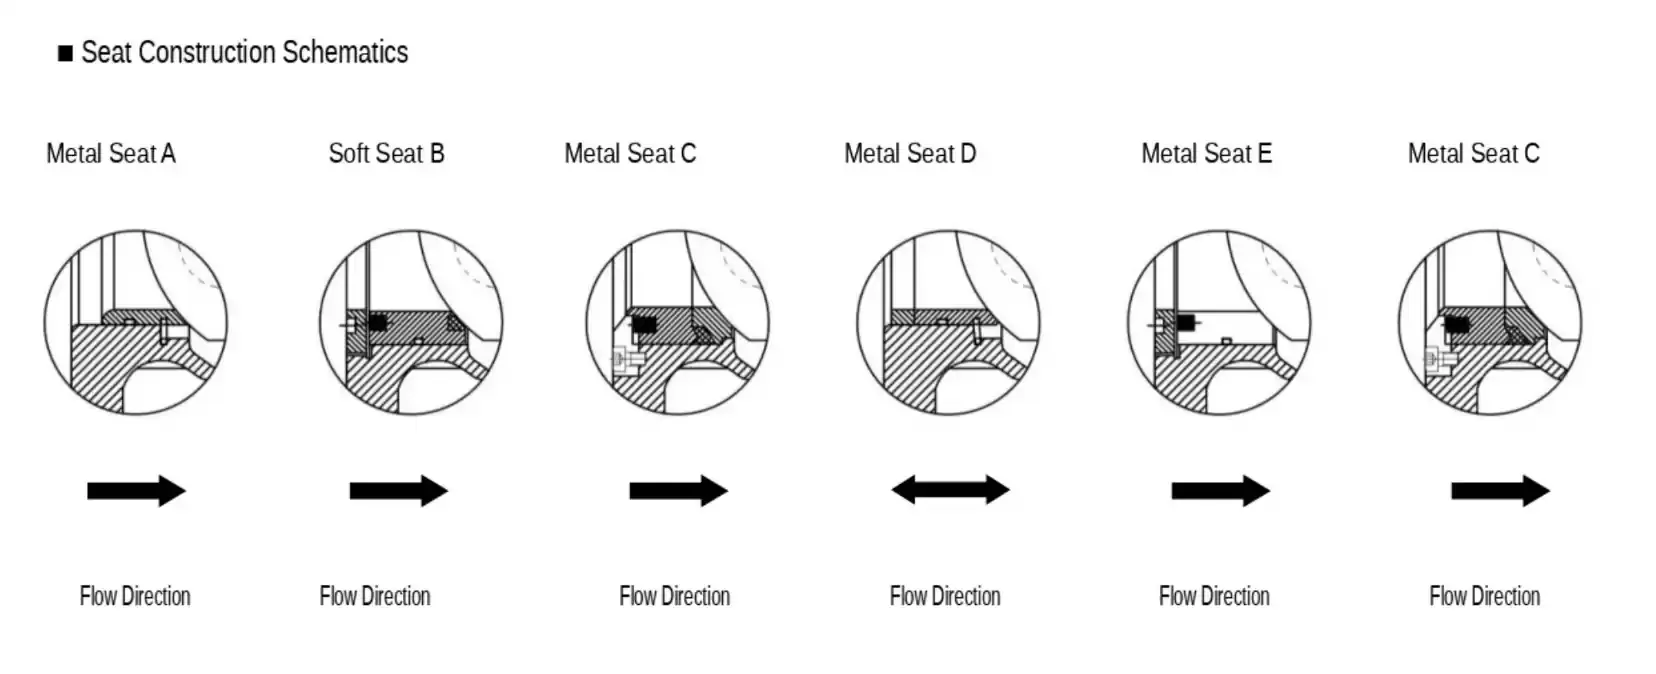
If the documents and physical markings do not agree, stop and resolve the difference before installation. Turning the valve around to suit access or pipe fit-up is not an acceptable correction. Upstream and downstream straight-pipe requirements must also come from the approved layout, valve design and manufacturer instructions. One fixed pipe-diameter rule does not apply to every control valve or service.
Confirm orientation and independent support
Check the permitted mounting position for the complete valve, actuator and positioner assembly. A vertical stem with the actuator above a horizontal line is common for many designs, but it is not a universal rule. Valve construction, actuator weight, drainage, process temperature and accessory limits may require another approved position. The exact orientation must follow the manufacturer instructions and project drawing.
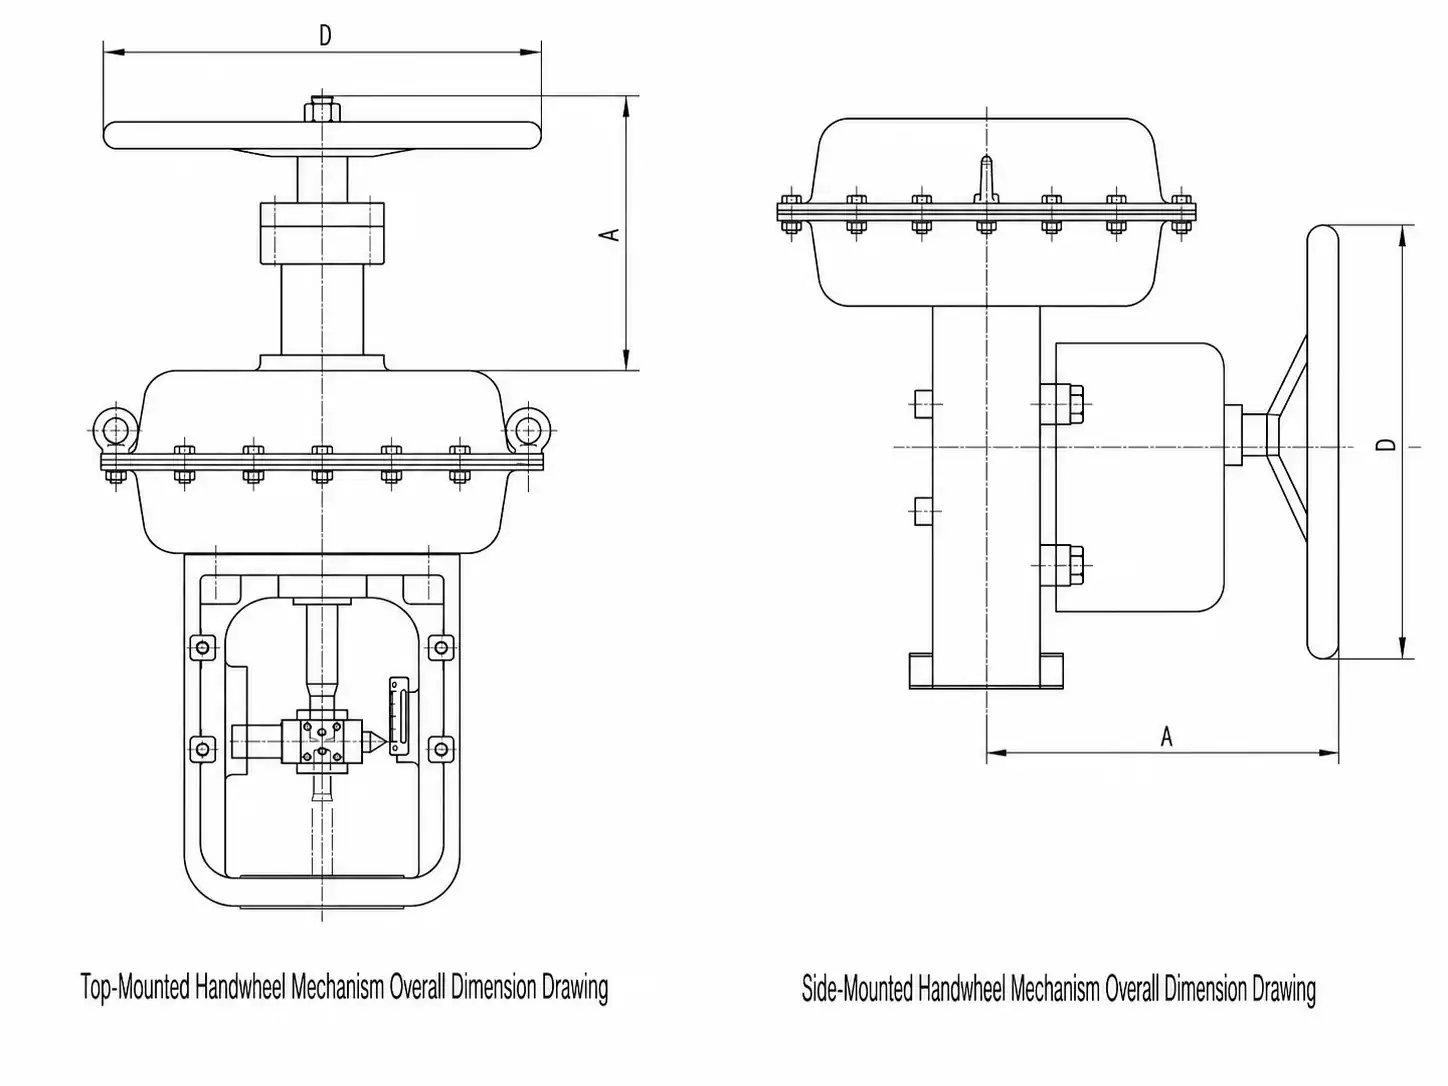
Use the following checks to keep external loads out of the installed valve package:
- Flange alignment: Keep the pipe ends parallel, centred and spaced for the specified gasket. Do not use the valve or flange bolts to pull misaligned pipework together.
- Pipe support: Carry the line weight and external loads without placing side load on the valve body, stem or shaft.
- Actuator support: Support a large or side-mounted actuator when required, without holding moving parts or stopping normal thermal movement.
- Lifting points: Do not lift or support the assembly by small-bore tubing, positioners, handwheels or other accessories.
Leave removal, access and environmental clearance
Check clearance through the valve’s full stroke, including the stem, shaft lever, handwheel and any external feedback linkage. The final arrangement must also allow access to the positioner, air filter regulator, solenoid valve and limit switches without removing nearby pipework.
Maintenance space should be checked with insulation, heat tracing, platforms, guards and cable routes in their final positions. Leave the removal space and lifting path stated in the installation drawing for the actuator, bonnet and trim. Keep actuator and accessory vents or exhausts clear, and apply the specified protection where heat, water, dust, vibration or corrosive air could affect the installed equipment.
Verify instrument air, electrical power and control signals
A command shown in the control room does not prove that the correct air pressure, electrical power or signal has reached the valve. Each supply must be checked at the field device against its nameplate, datasheet, wiring diagram and manufacturer instructions before the actuator is stroked.
Stabilise and leak-check the pneumatic supply path
Measure the instrument-air pressure at the valve package, not only at the main header. The pressure must remain within the limits of the actuator, positioner and connected accessories during both steady conditions and valve movement. A long or undersized tube, blocked filter, restricted fitting or overloaded air header may provide normal static pressure but allow it to fall during a full stroke.
Check the required air quality against the positioner and accessory instructions. Drain collected moisture where the design provides a drain, inspect the filter element and confirm that the regulator is set for the complete pneumatic package. There is no single pressure or air-quality class that suits every control valve.
Leak-check tubing, fittings, actuator connections and accessory manifolds using the approved site method. Trace the air path through the filter regulator, positioner, solenoid valve, booster or lock-up valve where fitted. Correct port connections matter because crossed actuator lines can reverse movement or cause a double-acting actuator to respond in the wrong direction.
Match voltage, signal type, range, polarity and I/O mapping
Verify the power supply at the device terminals before energising the circuit. The measured voltage, current type and polarity must match the positioner, solenoid valve, limit switches and other accessories. Do not assume that every valve uses the same voltage or a 4 to 20 mA command.
Trace the loop tag, cable number, terminal numbers and control-system input/output (I/O) assignment against the approved loop drawing and I/O list. Check that the controller output reaches the intended positioner and that each feedback or status signal returns to the correct control-system channel. Signal scaling, direct or reverse action and any split-range allocation must agree with the control narrative before calibration begins.
Grounding, cable shielding, barriers and segregation must follow the project electrical drawings and device instructions. In a hazardous area, confirm that the installed glands, plugs, barriers and equipment approvals match the defined protection method. An equipment approval does not correct an unsuitable cable entry or field connection.
Confirm vents, drains, cable entries and accessory states
Positioner, actuator, booster and solenoid exhaust paths must remain open and arranged as required by their installation instructions. A shipping plug left in an exhaust port can slow or stop valve movement. Open vents should also be protected from water, dust and blockage without restricting the designed exhaust flow.
Confirm the starting state of air isolation valves, electrical isolators, regulator settings, manual overrides, bypasses and lock-up devices against the approved commissioning procedure. Before applying a command, make sure the valve is released for movement, the process is in the required safe state and personnel are clear of the stem, lever and actuator linkage.
Calibrate the positioner and prove actual valve travel
The positioner must move the physical valve stem or shaft to the intended position and return matching feedback. A successful automatic calibration message checks the device routine, but it does not replace observation of the valve, actuator and feedback mechanism through the working range.
Set zero and span from the intended travel endpoints
Zero sets the lower end of the calibrated travel range, while span sets the distance between the lower and upper endpoints. These endpoints must come from the valve datasheet and control narrative. A low command does not always mean a closed valve because direct action, reverse action, split-range control and the specified fail action can change the required command-to-travel relationship.
Inspect the stem or shaft coupling, feedback arm, cam and local travel indicator before adjusting the positioner. Loose linkage or incorrect feedback geometry can make the displayed position differ from actual travel. Run the calibration with the process and movement area in the state required by the approved procedure, then confirm that the valve reaches its designed endpoints without forcing the actuator against an obstruction.
Mechanical travel stops protect the valve or actuator geometry and should not be moved merely to make the positioner display reach 0% or 100%. Any stop, linkage or zero adjustment must follow the exact valve, actuator and positioner instructions. The device-specific menu and adjustment sequence should be checked against the approved control valve positioner calibration procedure.
Check low, intermediate and high travel in both directions
Endpoint checks can miss errors that appear during normal throttling. At each approved test point, compare the following independent readings:
- Command signal: The intended input reaches the positioner.
- Physical travel: The stem or shaft reaches the corresponding mechanical position.
- Local indication: The valve or actuator indicator agrees with physical travel.
- Returned feedback: The control-system value agrees with the field position.
Intermediate checks can reveal incorrect feedback linkage, poor scaling or a restricted section of travel that an endpoint-only test will miss. Approach the same points from both opening and closing directions where the approved procedure permits. Record any delay, unstable motion or directional difference, then compare it with the project limits for error and repeatability.
Separate calibration error from mechanical or pneumatic limits
If the positioner receives the correct command but its output pressure does not change as expected, check its configuration, supply pressure, air restrictions and internal diagnostic messages. If output pressure changes but the stem or shaft does not follow, inspect the actuator connection, travel stops, packing friction, linkage and any mechanical obstruction.
When physical travel is correct but the control-system feedback is wrong, trace the feedback transmitter, positioner scaling and I/O mapping instead of recalibrating the actuator. The valve should be accepted only after command, actual travel, direction and returned feedback agree within the limits stated for that installed package.
Verify Fail Open or Fail Close under each defined loss condition
A Fail Open or Fail Close label is incomplete unless it identifies the event that causes the valve to fail. Loss of instrument air, loss of electrical power and loss of the control signal may produce different results because the positioner, solenoid valve, lock-up valve and actuator do not all respond to the same energy source.
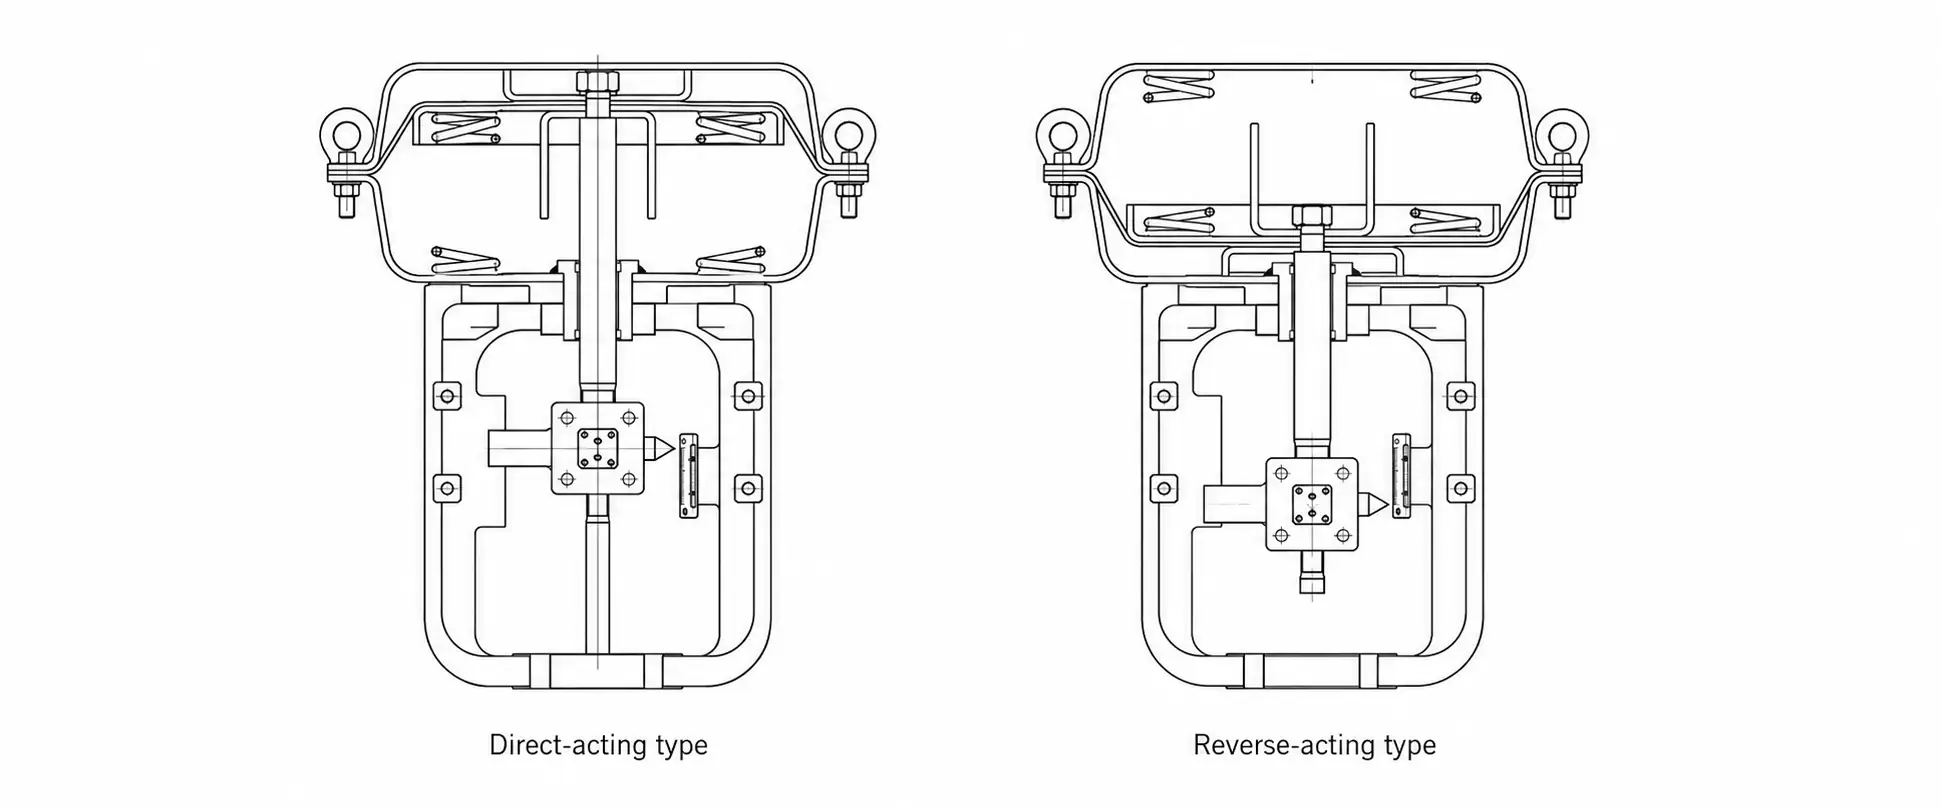
Actuator action alone does not determine the valve’s fail position.
Separate actuator action from package fail action
Air-to-open means that increasing actuator air pressure moves the valve towards the open position. Air-to-close means that increasing air pressure moves it towards closed. These terms describe actuator action; they do not by themselves prove the final position of the installed valve package.
A spring-return actuator may move towards its spring position when actuator pressure is removed. However, a solenoid valve can change the vent path, and a lock-up valve or volume tank may hold pressure instead of releasing it. A double-acting pneumatic actuator or electric actuator follows the failure logic provided by its control and stored-energy arrangement. The required result must therefore be taken from the datasheet, control narrative and cause-and-effect matrix, not inferred from the actuator label alone. The distinction is covered further in the guide to control valve air failure.
Test each loss condition separately
Place the process and valve in the safe state required by the approved commissioning procedure. Where the design distinguishes them, treat these as separate test cases:
- Loss of instrument air: Isolate air at the defined point and observe whether actuator pressure vents, remains locked or transfers to another supply.
- Loss of electrical power: Remove power from the positioner, solenoid valve or actuator at the point named in the procedure and observe the installed package.
- Loss of control signal: Remove or drive the signal to its defined failure state while device power remains available.
- Stored-energy response: For electric or electro-hydraulic actuators, confirm the designed action of the spring, battery, capacitor, accumulator, brake or last-position function.
Restore each energy source before applying the next test case and confirm the physical stem or shaft position rather than relying only on the control-system display. This separation shows whether the response comes from the actuator, positioner, solenoid valve, lock-up device or control-system logic.
Confirm the final position, movement time and recovery
For each test, record the starting position, failure event, direction of movement, actual final position and time taken to reach it. Compare these results with the project acceptance criteria. There is no universal fail-stroke time because actuator size, spring force, air capacity, accessory restrictions, valve load and process conditions all affect movement.
A workshop or no-load stroke confirms assembly direction but may not prove movement against process pressure, packing friction or other service loads. Any test under live process conditions requires an authorised site procedure, a defined safe process state and control of the resulting flow change. Do not perform an online fail stroke solely to complete a commissioning record.
After each failure test, restore the energy source and confirm the required recovery, alarm clearing and valve response. A correct valve fail position proves that part of the installed package response; it does not by itself prove the full safety instrumented function or its Safety Integrity Level.
Test the solenoid valve, limit switches and interlocks as one chain
A click from the solenoid valve coil or a status change on the control-system screen proves only one point in the shutdown chain. Commissioning must trace the command through the electrical output, solenoid valve, pneumatic path, actuator movement and field feedback, then confirm that the expected alarm or interlock state reaches the correct control-system input.
Prove the solenoid valve through the pneumatic path
Check the solenoid valve port connections against its pneumatic schematic before the functional test. Confirm the normal energised or de-energised state, because this depends on the shutdown design. The coil voltage, polarity and control-system output must match the device data, but electrical operation alone does not show that the internal spool has changed the air path.
Apply the approved command and observe the pressure at the solenoid inlet and actuator-side outlet. Confirm that the supply and exhaust paths change as designed and that the actuator moves in the required direction. A blocked exhaust, crossed port, sticking spool or closed isolation valve may allow the coil to operate without producing the required valve movement. Return any manual override to its normal position after the test. The functions and common arrangements are explained further in the guide to solenoid valves in control valve packages.
Set limit switches from the physical valve position
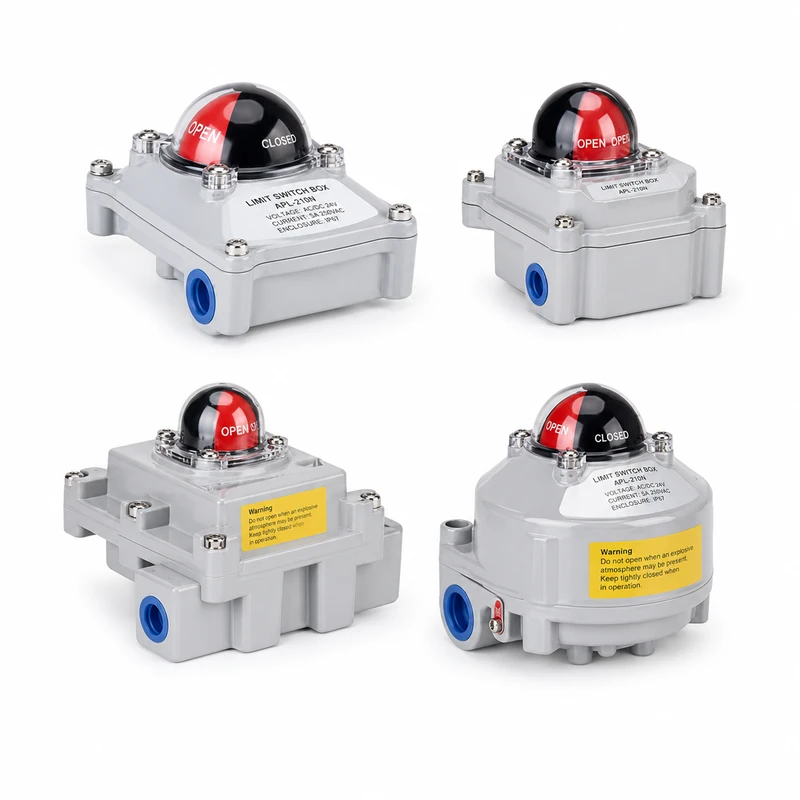
An open or closed limit switch provides a discrete position signal. It does not measure continuous travel and should not be treated as a substitute for positioner feedback. Set each switch or cam from the physical stem, shaft or lever position stated in the approved procedure, then check the contact state at the field terminals and the mapped control-system input.
The switch may be designed to change state before the valve reaches its mechanical stop, so there is no universal cam setting. Verify the required trip point and contact logic against the datasheet and cause-and-effect matrix. Confirm that the displayed Open and Closed labels are not reversed and that an intermediate valve position does not produce a false end-position indication. A related guide explains the difference between a valve positioner and limit switch.
Run the cause-and-effect test end to end
Use the approved cause-and-effect matrix to test each applicable trip, permissive and reset path. The process must be in the required safe state, and any test bypass must be authorised, identified and controlled.
- Establish the stated starting position and confirm the normal state of the solenoid valve, limit switches, interlocks, alarms and overrides.
- Apply the authorised initiating condition or simulated input at the point named in the test procedure.
- Verify the control-system logic and output, then measure the expected electrical state at the solenoid valve or actuator interface.
- Observe the pneumatic or electrical actuator response and confirm the valve’s physical direction, final position and movement time.
- Check that the correct limit switch, position feedback, alarm and interlock status return to the assigned control-system inputs.
- Reset the trip in the approved order, restore normal control and remove each temporary bypass or override under the site’s control procedure.
Repeat the sequence for each independent failure or interlock path that changes the valve response. Record the test conditions and any measured response time against the project acceptance criteria. Passing this functional chain proves only the tested cause and effect under those conditions; it does not by itself establish Safety Integrity Level performance or complete a safety instrumented function proof test.
Introduce process conditions and capture the first operating baseline
A pass mark without the test conditions is not a useful commissioning baseline. The first operating record should show how the installed valve package responds under a known command, process load and utility state. This as-left record, meaning the final accepted state after commissioning, gives maintenance teams a reference when the valve later becomes slow, unstable or unable to reach its required position.
Introduce process pressure and flow under controlled conditions
Place the valve in the starting position required by the approved plant start-up procedure. Introduce pressure, temperature and flow at the rate allowed for the piping system, valve materials and process equipment. The correct sequence may include warming, venting, draining or pressure balancing, so one fixed opening method should not be applied to every service.
As the process reaches stable conditions, inspect the body, bonnet, flange joints, packing area and instrument connections for external leakage. Watch the stem, shaft and actuator for unexpected movement, and note new noise, vibration or pressure changes. Stop or hold the start-up if the site procedure requires action for any unsafe leak, severe vibration or uncontrolled valve movement.
Compare the command signal, physical valve travel and returned position feedback while the valve is under process load. A valve that completed an unloaded stroke may respond differently when differential pressure, packing load and process forces act on the trim. Any online movement must remain within the operating limits and permissions set by the control room and commissioning procedure.
Save the as-left operating record
The baseline should identify the conditions around each result, not only the measured value. Use the fields that apply to the installed pneumatic, electric or electro-hydraulic package.
| Baseline item | What to record | Purpose of the record |
|---|---|---|
| Test context | Date, valve tag, operating mode and relevant process conditions | Supports comparison under similar conditions |
| Position response | Command, physical travel and returned feedback at the approved points | Shows later drift, deadband or travel loss |
| Actuator supply | Air supply and output pressure, or electrical and hydraulic values where available | Helps separate valve friction from utility problems |
| Movement time | Opening, closing and fail-stroke times under named test conditions | Reveals slower movement during later checks |
| Accessory chain | Solenoid state, limit-switch status, alarms and interlock results | Preserves the accepted cause-and-effect response |
| Physical condition | External leakage, packing condition, noise and vibration observations | Identifies changes from first service |
| Device diagnostics | Health status, alerts and signature or trend data when supported | Provides a device-specific comparison point |
Record the units, test method and acceptance source for each measured value. Stroke time, actuator pressure and diagnostic data should not be compared without checking whether the process load, supply conditions and test method were similar. Diagnostic signatures support condition comparison, but they do not guarantee a fixed service life.
Do not record a seat-leakage class as accepted from an informal online observation. A valid seat-leakage result needs the applicable test method, pressure, medium, flow direction and acceptance limit. Once the operating baseline is stored, it can support faster control valve troubleshooting when later performance differs from the as-left condition.
Conclusion
Control valve commissioning is complete when the installed package reaches each commanded position, moves to the specified failure position under every defined loss condition, and returns the correct feedback through the actual accessory and interlock chain. Saving these results with the test conditions creates an as-left reference that supports a clear handover and gives future maintenance work a measured baseline instead of a simple pass mark.