

A calendar date can trigger a review, but it cannot tell a maintenance team what to inspect. The scope must reflect the process medium, pressure drop across the valve, cycle count and travel pattern, required shut-off leakage performance, cavitation risk, and failure history. Each factor points to different damage paths and parts that may need attention.
Site rules, legal duties, and manufacturer instructions may still set minimum review points. Within those limits, current operating evidence should decide whether the valve needs online and external condition checks, planned functional checks, or an isolated internal inspection. Fixed dates remain useful triggers, while service exposure, condition trends, and repeat faults determine how far the inspection should go.
Control Valve Preventive Maintenance Is a Scope Decision
A preventive maintenance plan makes two related decisions:
- Review trigger: define what starts the review, such as a site requirement, operating change, alarm, condition trend, or past fault.
- Inspection scope: choose the level of work that matches the evidence and the consequence if the valve loses control or fails to shut off as required.
Online and external checks are the lowest-disturbance option. They can cover leakage, air supply, command and travel signals, noise, vibration, and visible condition without opening the valve. A planned functional check adds controlled movement or a defined performance test. Isolated internal inspection is used when the evidence points to seat, trim, stem, guide, body, packing, or actuator damage that cannot be confirmed from outside.
The action threshold is the point at which the evidence justifies a deeper inspection. A repeated travel deviation on a shutdown-critical valve may need earlier action than the same deviation on a less critical valve in stable service. Criticality does not prove damage, but it changes how much uncertainty the site can accept before further checks are required.
When a symptom has not yet been tied to the valve, the wider control valve troubleshooting and maintenance resources can help separate signal, air, actuator, valve, and process causes before the inspection scope is widened.
Six Factors That Change the Inspection Scope
Each risk factor points to a different failure path and group of parts. Use these factors to direct the inspection instead of applying the same tasks to every control valve.
Medium, solids and contamination
The process medium changes where deposits, corrosion, erosion, blockage, or sticking may develop. Fluid chemistry and phase matter, but so do solids, viscosity, crystallisation, and contaminants carried into small trim passages. These conditions can expand the scope to the packing, stem or shaft, guides, seat, trim, body surfaces, and narrow flow paths. Contaminated instrument air creates a separate fault path and shifts attention towards the filter regulator, tubing, positioner, and actuator.
The fluid name alone does not support a material, cleaning, or lubricant decision. Those choices need the actual composition, concentration, temperature, and valve construction.
Pressure drop and operating range
Pressure drop across the valve should be reviewed for normal operation, start-up, shutdown, and known upset cases. A high or changing pressure drop can increase actuator load, trim velocity, noise, and wear. Operation near a small opening may also keep the same part of the trim exposed to high local velocity. Slow travel, position error, or poor control under these conditions can justify checks of actuator output, linkage, stem or shaft movement, and trim condition.
Pressure drop must be read with upstream pressure, downstream pressure, flow, and valve travel. A large pressure drop alone does not prove cavitation or identify the damaged part.
Cycle count and travel pattern
A cycle counter records activity, but it does not show how much load each movement placed on the valve. Ten thousand short corrections around one travel point differ from ten thousand full movements under a high or changing pressure drop. Reversals, total travel, dwell time, movement close to the seat, and loaded start-stop events give the count useful context.
A rising cycle or travel total can help rank valves for review. It cannot prove packing, guide, seat, linkage, or actuator wear without a change in performance, inspection evidence, or relevant failure history.
Leakage class and shut-off duty
External leakage and downstream passing require different checks. Leakage around the packing, bonnet joint, tubing, or actuator is visible outside the pressure boundary. Downstream passing points towards the closure system, but possible causes include seat or trim damage, deposits, poor alignment, limited actuator force, or a positioner and linkage problem.
The required leakage class changes the acceptance basis for shut-off duty. Any comparison must keep the test medium, test pressure, flow direction, closing force, temperature, and test method attached to the result. A valve that passes a bench test under one defined method is not proven healthy under every installed service condition.
Cavitation, noise and vibration risk
In liquid service, cavitation can begin when local pressure inside the valve falls below the liquid vapour pressure and bubbles form. If pressure then recovers above the vapour pressure, the bubbles collapse. This collapse can damage the trim, seat, body, and nearby downstream surfaces, depending on where pressure recovery occurs.
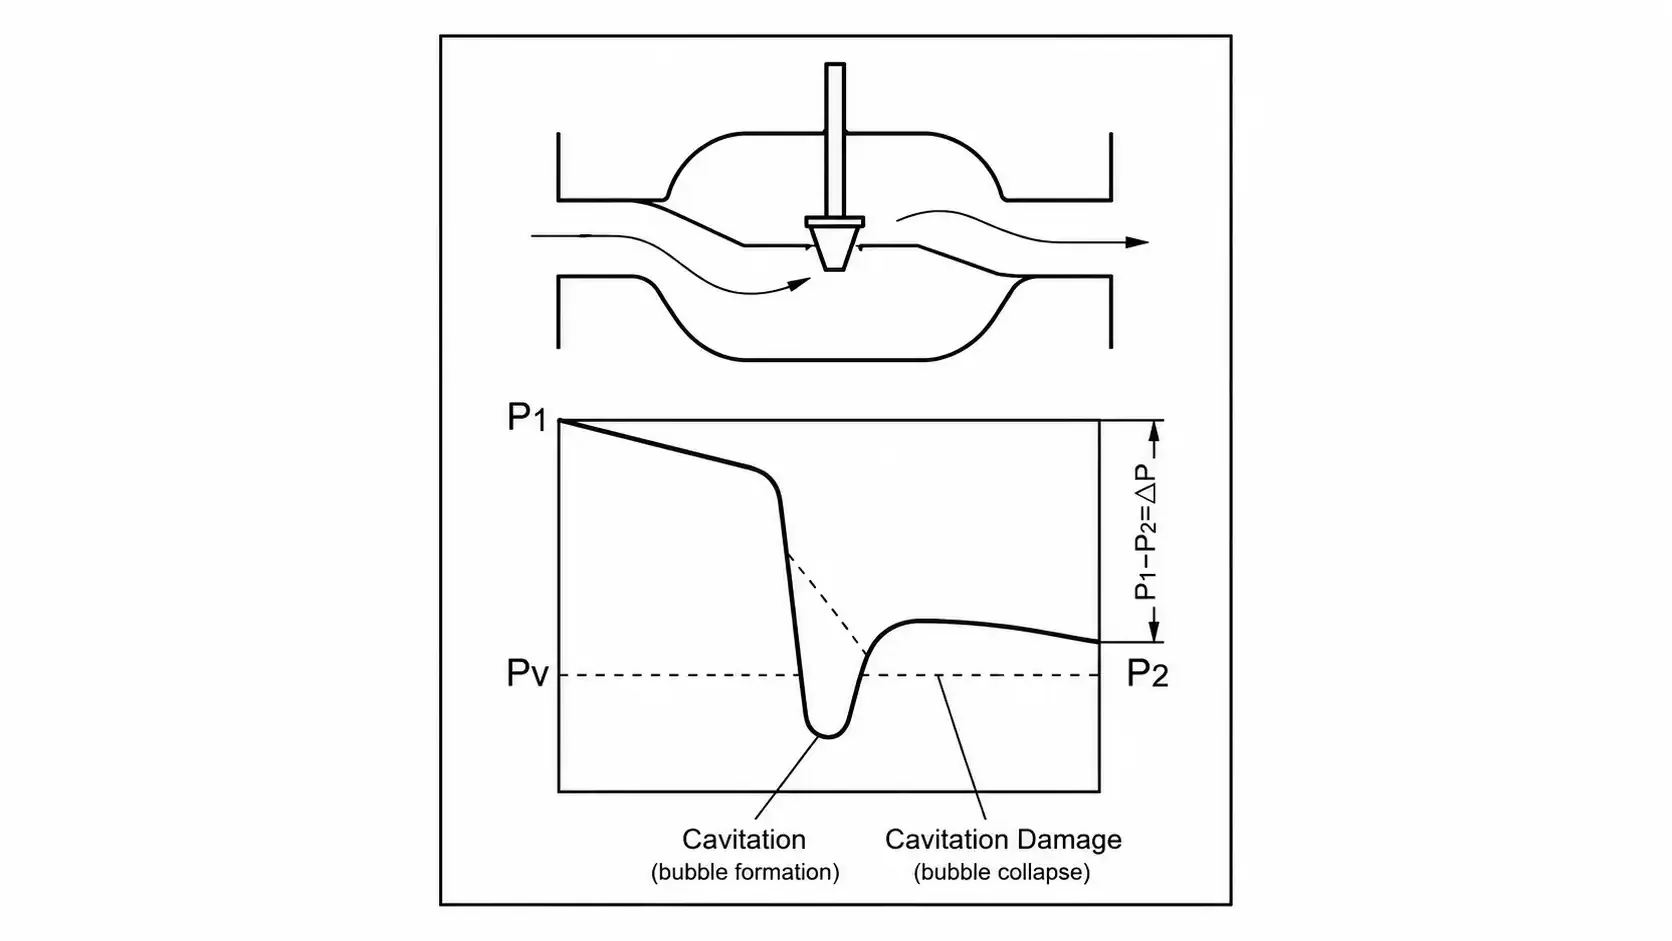
New noise or vibration can support a cavitation review, but neither signal proves the cause alone. Pressure, flow, travel, process stability, and past damage should be reviewed together. When the evidence supports cavitation risk, the scope should include installed operating conditions as well as internal and downstream surfaces. The guide to how cavitation and flashing change the pressure profile covers the mechanism in more detail.
Failure history and repeat damage
Repeated maintenance on the same part can show that the previous inspection scope was too narrow. Frequent packing adjustment, recurring calibration drift, repeated air leaks, another seat repair, or renewed trim damage should widen the fault search beyond the part last replaced. A change in medium, pressure drop, control duty, or operating range may also explain why an earlier repair did not hold.
History helps form better fault paths, but it does not prove one root cause. Similar faults across several valve tags may point to a shared air, process, installation, or operating issue. The maintenance team can use a wider method to separate the symptom from the fault source.
The following matrix shows how service evidence can expand the inspection scope without creating a fixed maintenance interval.
| Factor | Evidence That May Expand the Scope | Areas to Examine |
|---|---|---|
| Medium and contamination | New solids, deposits, corrosion marks, sticking, or contaminated instrument air | Packing, stem or shaft, guides, trim passages, body surfaces, and air system |
| Pressure drop | High or changing pressure drop, low travel at high flow, or slow response under load | Actuator output, linkage, travel response, trim, seat, and downstream condition |
| Cycle and travel duty | More reversals, narrow-band movement, seat-area movement, or loaded start-stop events | Packing, stem or shaft, guides, linkage, seat, trim, and actuator wear points |
| Leakage duty | External leakage or rising downstream passing under the same test basis | Packing and joints, or seat, trim, alignment, actuator closure, and leak test |
| Cavitation risk | New noise or vibration with pressure-recovery evidence, unstable performance, or past pitting | Pressure and flow review, trim, seat, body, and downstream surfaces |
| Failure history | Repeat faults, continued calibration drift, repeated part replacement, or similar faults across tags | Process, signal, air, actuator, valve, and past test evidence beyond the replaced part |
No row sets an inspection interval by itself. A factor should expand the scope when the service condition, condition trend, failure evidence, or process consequence shows that the current level of checking leaves too much uncertainty.
Turn Risk Factors Into Inspection Triggers
An inspection trigger becomes useful when it connects a change in evidence to a named maintenance action. Medium, pressure drop, cycling, leakage duty, cavitation risk, and history set the areas of concern. Current condition, the size of the change, and the process consequence decide whether the scope should remain online or move deeper.
Set a known-good baseline
A known-good baseline records how the control valve behaved after commissioning or an accepted repair. Depending on the equipment and available diagnostics, it may include:
- Valve response: command and travel response, together with stroke time.
- Pneumatic condition: air supply and available positioner output data.
- Mechanical condition: friction or valve-signature data where available.
- Shut-off performance: leakage results with the test conditions and acceptance method.
- Process reference: normal upstream pressure, downstream pressure, flow, and valve travel.
The baseline belongs to the configuration and test conditions under which it was recorded. A change in positioner settings, actuator setup, packing adjustment, trim, process medium, or test method can make an older result unsuitable for direct comparison. Undocumented readings should not be treated as a known-good reference.
Later evidence is easier to interpret when the control loop is separated into signal, air supply, positioner, actuator, valve, and process zones. This prevents a travel or flow problem from being assigned to the valve body before the rest of the chain has been checked.
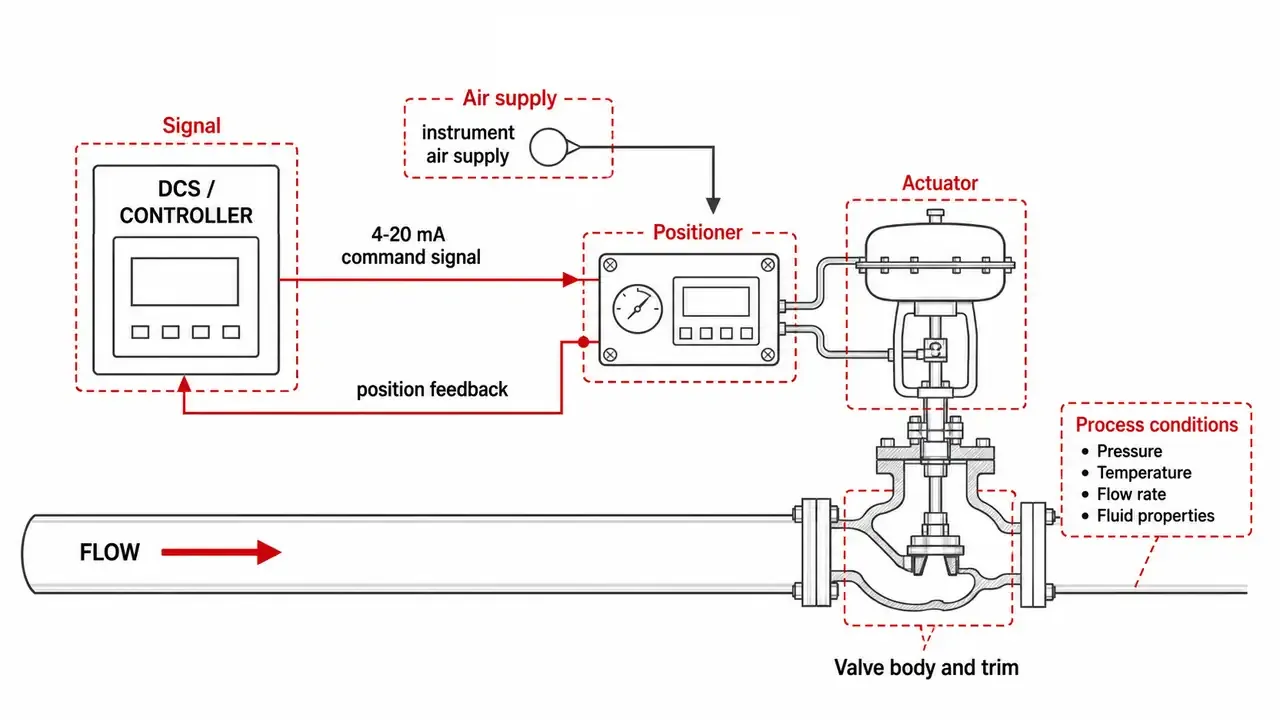
Use online evidence before disturbing the valve
Online evidence can narrow the fault zone while the control valve remains in service. Comparing the command with travel feedback can show whether movement follows the signal. Air supply and positioner output can expose a pneumatic limit, while travel deviation, response time, friction trend, cycle count, noise, vibration, leakage, and process trends can show where further checks may be useful.
Not every control valve provides every diagnostic value. Available data should be compared with a valid baseline and the current operating condition. Control valve diagnostic data acquisition and reporting is separate from condition interpretation. A diagnostic reading can guide the inspection, but it does not prove the internal condition of the seat, trim, guides, or body.
Escalate on change, not on one reading
A single reading may reflect process movement, test conditions, instrument error, or a short disturbance. A deeper inspection is better supported by one or more of these evidence changes:
- Persistent deviation: performance remains outside the valid baseline under comparable conditions.
- Repeated warning: an alarm returns or the valve response continues to worsen.
- Performance loss: the valve loses control or breaches a defined acceptance limit.
- Recurring fault: the same leakage, sticking, calibration, air, or trim problem returns after maintenance.
A new medium, higher pressure drop, changed travel pattern, tighter shut-off duty, or higher process consequence can also move the action threshold. The threshold should come from the valid baseline, manufacturer or project acceptance limits, site risk policy, and applicable rules. A made-up condition score or universal percentage change cannot replace those boundaries.
Site procedures, manufacturer instructions, and legal requirements may require action even when the condition trend appears stable. These requirements set minimum controls, while the evidence determines which parts and tests should be added to the inspection.
Choose the Right Inspection Scope
Use the smallest safe inspection scope that can resolve the current evidence and meet the applicable acceptance requirement. Starting with external checks can avoid unnecessary valve disturbance. The scope should move deeper when those checks cannot explain a worsening trend, repeated fault, loss of function, or unacceptable process risk.
Online and external condition checks
Online and external checks suit initial fault screening and valves whose condition remains stable against the baseline. The work can cover visible leakage paths, mounting and fasteners, actuator linkage, instrument tubing, air supply, environmental exposure, command and travel signals, alarms, noise, vibration, and related process trends.
Each check should follow the suspected damage or fault path. A valve exposed to wet or dirty instrument air needs different attention from one showing rising downstream leakage or a response change under high pressure drop. A sound external condition does not prove that the seat, trim, guides, or internal body surfaces are free from wear or deposits.
Planned functional checks
A planned functional check is useful when online evidence shows a movement or performance problem that cannot yet be placed in the signal, air, actuator, valve, or process zone. Under an approved site procedure, controlled movement may be used to compare command with travel, check response and stroke time, review calibration, assess air-supply recovery, or test fail action where it applies.
The test objective, allowed movement, process condition, and acceptance limit must be set before the check begins. A standard series of fixed travel points is not suitable for every installed valve because process disturbance, valve load, available travel, and safety duties differ. Leakage checks also need a named method, test medium, pressure, flow direction, and closing condition if the result will be compared with an earlier test.
Isolated internal inspection and repair
Internal inspection is justified when the evidence points to deposits, seat or trim damage, stem or guide wear, packing problems, corrosion, erosion, cavitation, body damage, or an actuator fault that cannot be confirmed from outside. The first task after access is to preserve the evidence. Deposits, wear location, pitting, damaged edges, alignment, and failed seals should be recorded before cleaning or repair removes clues about the failure path.
Intrusive work must wait until the valve and actuator are covered by the site’s authorised isolation, depressurisation, stored-energy control, and verification procedure. Pneumatic, hydraulic, electrical, spring, process-pressure, thermal, and gravity hazards may require different controls.
Inspection findings can define the repair scope, but exact clearances, surface limits, packing methods, and actuator settings should come from the applicable equipment instructions and approved repair procedure. This article does not support live repacking, disassembly, manual stroking, or bypass work without those controls.
| Inspection Level | Typical Trigger | Scope | Decision Output |
|---|---|---|---|
| Online and external | Stable condition, scheduled review point, or first sign of change | Visible condition, air and signal path, command and travel, alarms, and process trends | Continue monitoring or define a functional test |
| Planned functional | Repeated deviation, unclear response fault, alarm, or defined performance concern | Approved movement, response, calibration, air recovery, fail action, or defined leakage check | Accept the condition, correct an external cause, or justify isolation |
| Isolated internal | Evidence of internal damage, unacceptable leakage, recurring failure, or unresolved high-consequence risk | Seat, trim, body, outlet, packing, stem or shaft, guides, actuator, deposits, and damage evidence | Confirmed findings, repair basis, and a new acceptance record |
These levels are not a fixed sequence. Strong evidence of internal damage may justify direct escalation to an isolated inspection, while a stable valve may remain at the online level. The selected scope should close the main evidence gap without adding work that does not change the maintenance decision.
Make Each Maintenance Result Improve the Next Scope
A useful maintenance record shows what was found, what changed, and the conditions under which the control valve passed its final checks.
- As-found condition: record the fault zone, damage location, deposits, wear pattern, and observed failure mechanism without claiming an unproven root cause.
- Work completed: record repaired, replaced, or adjusted parts, changed settings, and the final trim, packing, actuator, and positioner configuration.
- As-left condition: record the acceptance method, test conditions, result, and new baseline. A bench or functional test proves performance only within those recorded conditions.
After accepted work, compare command and travel response, friction data where available, stroke time, leakage, air supply, and process behaviour with the new baseline. If the trim, packing, actuator, or positioner configuration changes, the older baseline may no longer support a direct comparison.
If the same fault returns, expand the next inspection beyond the part previously repaired. Similar faults across several valve tags may point to a shared process, instrument-air, operating, or maintenance issue. A clean result can narrow the next area of concern, but it does not by itself justify a longer maintenance interval.
Conclusion
Treat the maintenance plan as a controlled feedback loop. Site, legal, and manufacturer requirements set the minimum review points, while medium, pressure drop, cycle and travel duty, shut-off need, cavitation exposure, current condition, and failure history decide the inspection scope. Preserve each result with its test conditions and reset the baseline after accepted work, so repeated evidence rather than a universal calendar widens the next scope.