

A pneumatic butterfly valve combines a quarter-turn butterfly valve with an air-powered rotary actuator. Compressed air moves the actuator, the actuator turns the valve shaft, and the shaft rotates the disc to start, stop, or adjust flow.
The valve body, actuator, fail position, air supply and control accessories must be treated as one package. A suitable valve body can still perform poorly if the actuator cannot deliver enough torque at the lowest air pressure, or if the selected fail action does not match the process risk.

What is a pneumatic butterfly valve?
A butterfly valve controls process flow with a circular disc mounted on a shaft. The disc turns through about 90 degrees between the open and closed positions. Adding a pneumatic rotary actuator allows this movement to be controlled by compressed air instead of a manual lever or gearbox.

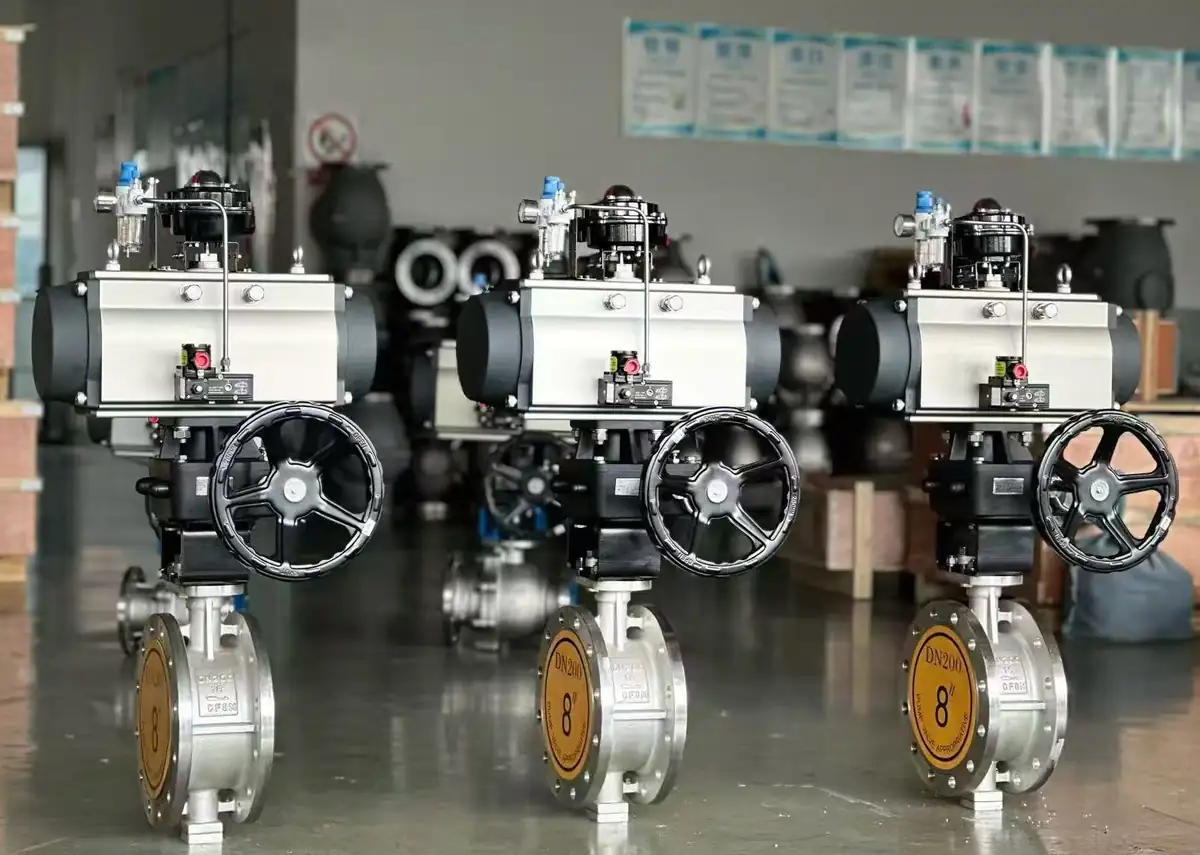
A complete pneumatic butterfly valve may also include a solenoid valve, positioner, air filter regulator, speed controls, limit switches and a position indicator. These parts do different jobs. The actuator creates torque, the solenoid directs air for on-off movement, and the positioner corrects valve position during modulating control.
The term therefore describes an assembled control package rather than one valve part. Its performance depends on the mechanical connection between the actuator and shaft, the available air pressure, the valve torque and the way the accessories control or exhaust air.
How does a pneumatic butterfly valve work?
From control signal to disc rotation
In an on-off assembly, an electrical or pneumatic command changes the air path to the actuator. The same motion chain applies to rack-and-pinion, scotch-yoke and other rotary mechanisms, although their torque curves are different.
- The control system sends a command. A switch, programmable logic controller or process-control system requests the valve to open, close or move to a set position.
- The air-control device changes the flow path. A solenoid valve directs compressed air to the required actuator chamber and vents the other chamber where the circuit design requires it.
- The actuator converts air pressure into rotary torque. Pistons or vanes move inside the actuator and turn its output drive.
- The shaft rotates the disc. The actuator drive transfers torque through the mounting and coupling into the butterfly-valve shaft.
- The disc changes the process-flow area. A disc aligned closer to the pipe axis gives a larger flow area; rotating it towards the seat reduces the area and finally closes the valve.

The torque needed to begin opening is often different from the torque needed through mid-stroke or near the seat. For this reason, actuator selection must use the valve’s torque demand across the full travel rather than one general torque value. The mechanism is covered in more detail in the guide to how pneumatic rotary actuators work.
What happens when the air supply is lost?
A spring-return actuator stores energy in its springs during the powered stroke. When the air supply is removed, the springs drive the actuator towards its preset position. The assembly reaches that position only when the spring torque remains higher than the valve and process torque at each required point in the return stroke.
A double-acting actuator uses air for both directions and has no built-in spring-return position. After air loss, its final position depends on the pneumatic circuit, internal leakage, process torque and any added air-lock or storage device. Trapped air may hold the valve for a time, but this should not be treated as a defined fail position unless the complete package is designed and verified for that duty.
Fail-open, fail-closed and fail-in-place are process-safety decisions. The correct choice follows the consequence of losing cooling, fuel, feed, venting or isolation, not the label on the actuator. See the detailed comparison of fail-open and fail-closed valves.
Spring-return vs double-acting actuators
The actuator action changes air use, available torque, package size and air-loss behaviour. Neither design is the better choice for every pneumatic butterfly valve.
| Selection point | Spring-return | Double-acting |
|---|---|---|
| Powered movement | Air drives one direction; springs drive the return. | Air drives both directions. |
| Loss of air | Moves towards the spring position when the package is correctly sized. | Has no inherent return position. |
| Torque check | Check air and spring torque at all required stroke points. | Check output in both powered directions. |
| Package size | May need a larger actuator because air must work against the springs. | May provide the required torque with a smaller actuator. |
| Typical decision | Use when a defined mechanical return position is required. | Use when powered movement in both directions suits the control and failure strategy. |
The table describes actuator behaviour, not the final safety function by itself. Valve torque, actuator orientation, spring set, mounting, air circuit and process forces can all change the result. The separate guide to single-acting and double-acting pneumatic actuators covers this distinction in more depth.
Which butterfly valve construction fits the duty?
Wafer, lug and flanged connections
A wafer butterfly valve is clamped between two pipe flanges. It gives a short face-to-face length and low package weight, but the valve does not normally provide its own fully bolted end connection. A lug valve has threaded lugs around the body. Some lug designs can support removal of piping on one side, but only when the manufacturer’s dead-end rating, flange arrangement and bolting allow it.
A flanged butterfly valve has integral flanges and gives a more rigid pipe connection, with added weight and space. The connection choice affects installation, pipe support and maintenance access before it changes flow performance. The differences are covered in lug vs wafer butterfly valves and the guide to butterfly valve end connection types.
Concentric, double-offset and triple-offset designs
In a concentric butterfly valve, the shaft passes through the centre of the disc and the disc stays in contact with the resilient seat during much of the stroke. This simple layout is compact and often suits compatible water, air and general liquid services. Seat friction can form a large part of the required operating torque.
A double-offset design moves the shaft away from both the disc centreline and the seat plane. The disc lifts away from the seat sooner during opening, which reduces rubbing. The result can support more demanding cycling, pressure or temperature duties, but the actual limit still follows the seat design, body rating and manufacturer data.
A triple-offset valve adds an angular offset to create a cam-like sealing movement. Metal-seated versions are often considered where temperature, cycling or resilient-seat wear changes the choice. Metal seating does not by itself prove a particular shutoff class or leakage result; the valve design and stated test basis remain decisive.
Seat and wetted-material compatibility
The process medium contacts more than the valve body. The disc, shaft, seat, packing and seals can each set the service limit. Four conditions commonly change the material decision:
- Medium chemistry: can swell, harden, dissolve or corrode an exposed material.
- Temperature: changes seat strength, sealing force and chemical resistance.
- Solids: can cut a soft seat, score the disc edge and raise operating torque.
- Cleaning conditions: can expose the valve to chemicals or temperatures that differ from the normal process.
EPDM often fits water and many aqueous duties but is generally a poor choice for mineral oils. NBR is often considered for oils but has its own chemical and temperature limits. PTFE offers broad chemical resistance, although pressure, temperature, cold flow and the supporting seat design still matter. A metal seat may extend the usable temperature or erosion range, but it does not guarantee bubble-tight shutoff.
MacoTango lists separate pneumatic soft-seal butterfly valve, pneumatic high-performance butterfly valve and pneumatic metal-seated butterfly valve families. These construction labels narrow the options, but the current datasheet and service conditions must decide the final operating limits.
On-off vs modulating control
On-off packages
An on-off package moves between defined open and closed positions. A solenoid valve directs the air, while limit switches or a position indicator report whether the actuator reached the commanded end position. Flow controls may restrict the actuator exhaust to adjust stroke speed. They do not change the valve’s torque requirement or prove that the disc reached its seat.
Fast operation is useful for some isolation and sequencing duties, but faster is not always safer. Closing a liquid line too quickly can create a pressure surge. The required stroke time must match the piping system, not just the actuator’s no-load speed.
Modulating packages
A modulating package moves the disc to intermediate positions. A positioner compares the control signal with actual shaft position and meters air to reduce the error. The positioner, actuator, linkage and valve must have enough resolution and low enough friction to respond without repeated overshoot or sticking.
Disc position is not the same as flow control quality. A butterfly valve has a non-linear relationship between disc angle and flow area, and the installed piping pressure drop changes the final response. Near the closed position, a small angle change can cause a large change in velocity or flow. High differential pressure can also raise noise, erosion or cavitation risk in liquid service.
Where the duty needs stable throttling rather than simple isolation, review the valve’s installed behaviour and operating range through the guide to butterfly valves for flow control.
How to size the actuator without guessing
Match break, running and reseating torque
The actuator must cover the highest required valve torque at the corresponding point and direction of travel. Break torque starts movement from the seat. Running torque covers the mid-stroke movement, where process flow can add dynamic torque. Reseating or end torque returns the disc to the required shutoff position.
These values change with valve size, seat design, differential pressure, temperature, medium, deposits, wear and time between cycles. A general torque value from another butterfly valve is not a sound basis for sizing. Use the valve manufacturer’s torque data for the actual construction and duty.
Size at the minimum credible air supply
Pneumatic actuator output falls when the available air pressure falls. Selection should therefore use the lowest pressure that can reach the actuator during real plant operation, after allowing for regulator setting and pressure losses. Nominal compressor pressure at another part of the system may not represent the pressure at the actuator during a stroke.
For a spring-return actuator, compare air and spring torque with the matching valve torque at each required travel point. For a double-acting actuator, check both powered directions. Then confirm that actuator output at the highest possible supply pressure does not exceed the valve’s maximum allowed stem or shaft torque. A fixed safety percentage cannot replace these checks.
The full method is covered in the pneumatic actuator sizing guide.
Check stroke time and accessory restrictions
Actuator size alone does not set operating speed. Solenoid flow capacity, tube bore, fitting restrictions, air pressure, actuator chamber volume, speed controls and exhaust paths all affect stroke time. A booster or quick-exhaust valve may increase speed where the process requires it, but the piping system and valve mechanics must tolerate the faster movement.
Clean, dry instrument air also affects repeatability and service life. Water, oil, particles or icing can restrict small passages, damage seals and cause slow or uneven movement. Air preparation is part of the valve package, not a separate housekeeping detail.
Where pneumatic butterfly valves work well and where they do not
A pneumatic butterfly valve is often a good fit when the process needs:
- Compact automated isolation: especially where line size makes a quarter-turn butterfly valve lighter than many alternative valve bodies.
- Frequent or remote operation: where suitable instrument air and control signals are already available.
- A defined mechanical return: when a correctly sized spring-return package can move the valve to the required fail position.
- Moderate throttling: where the selected valve construction, pressure drop and control range support stable disc positioning.
Closer review is needed under these conditions:
- High differential pressure during throttling: can increase dynamic torque, velocity, noise, erosion or cavitation risk.
- Abrasive or fibrous solids: can damage the seat, collect around the disc or prevent full closure.
- Demanding shutoff or high temperature: requires a verified seat design, leakage basis and material limit.
- Poor air quality or unstable pressure: can reduce actuator torque and make movement slow or erratic.
- Very fast liquid-line closure: can produce a pressure surge even when the valve and actuator operate as commanded.
This service-based check is more useful than choosing from a broad industry label. Two water systems can need different seats, fail positions and stroke times, while two chemical duties in the same plant may require different wetted materials.
A practical pneumatic butterfly valve selection sequence
- Define the valve duty and failure consequence. Decide whether the valve provides isolation or modulation, then establish the required position after loss of air or power.
- Choose the valve construction. Match the connection, concentric or offset geometry, pressure rating and wetted materials to the process and maintenance needs.
- Establish torque demand across the stroke. Use break, running and reseating data that reflect the valve, differential pressure, seat and service condition.
- Select the actuator over the real air-pressure range. Check every required air and spring torque point at minimum supply, then verify the maximum allowed shaft torque at the highest supply.
- Complete and verify the control package. Match the solenoid or positioner, feedback, tubing, air preparation, stroke time, mounting and coupling to the intended on-off or modulating function.
Conclusion
A pneumatic butterfly valve should be selected as a complete operating package. The body and seat must suit the process, the actuator must cover the full torque demand, and the air circuit must deliver the intended movement and fail response. MacoTango’s pneumatic valve range provides the relevant construction families after these technical choices have been made.