

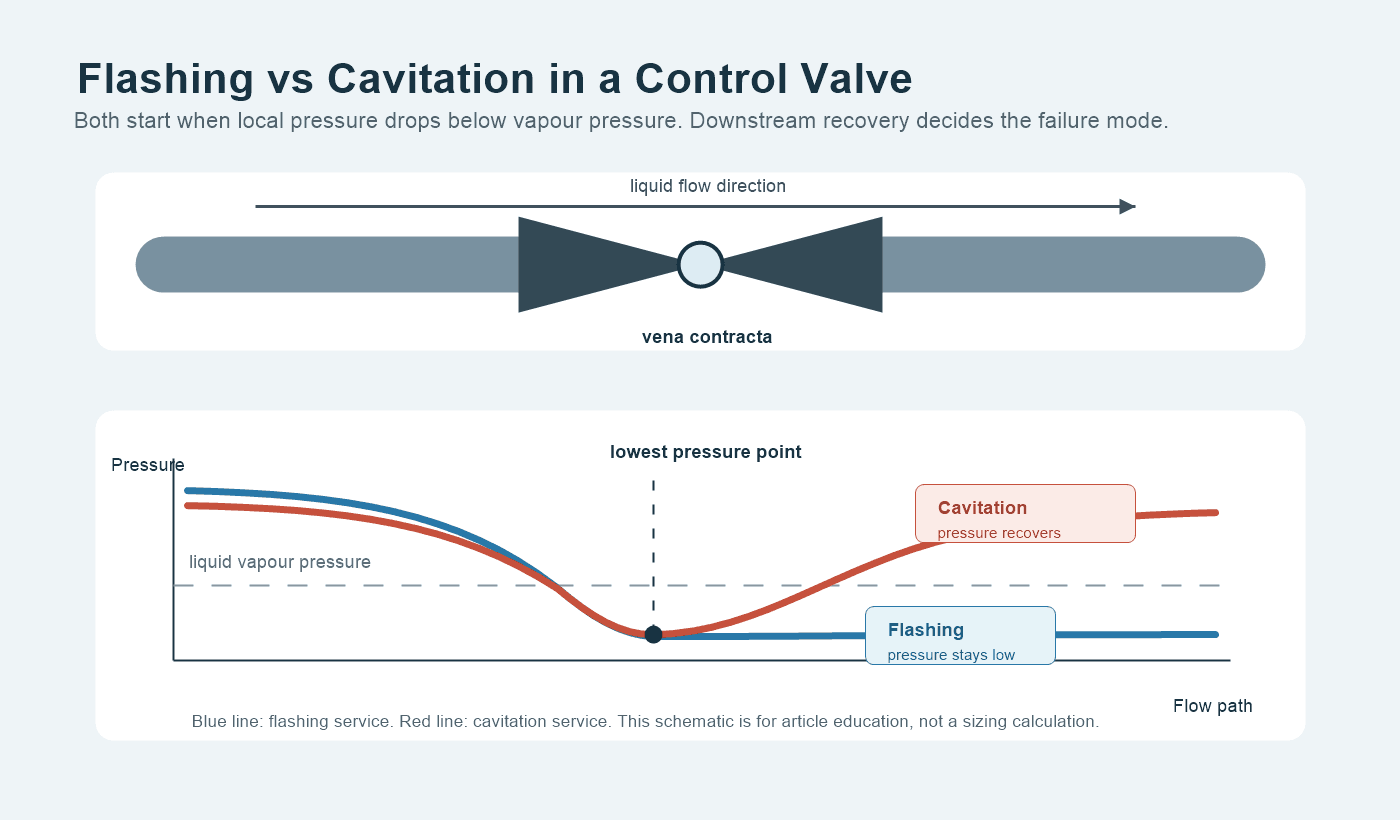
Flashing and cavitation both begin when liquid pressure falls below the liquid’s vapour pressure at the valve restriction. The difference appears downstream. In cavitation service, pressure recovers above vapour pressure and the vapour bubbles collapse. In flashing service, downstream pressure stays below vapour pressure, so the vapour remains in the flow.
Erosion is a separate mechanical wear process. High velocity, entrained solids, or a two-phase jet can remove metal without bubble collapse. Cavitation, flashing, erosion, and corrosion may also act together, so a damaged plug or seat should not be labelled as cavitation from appearance alone.
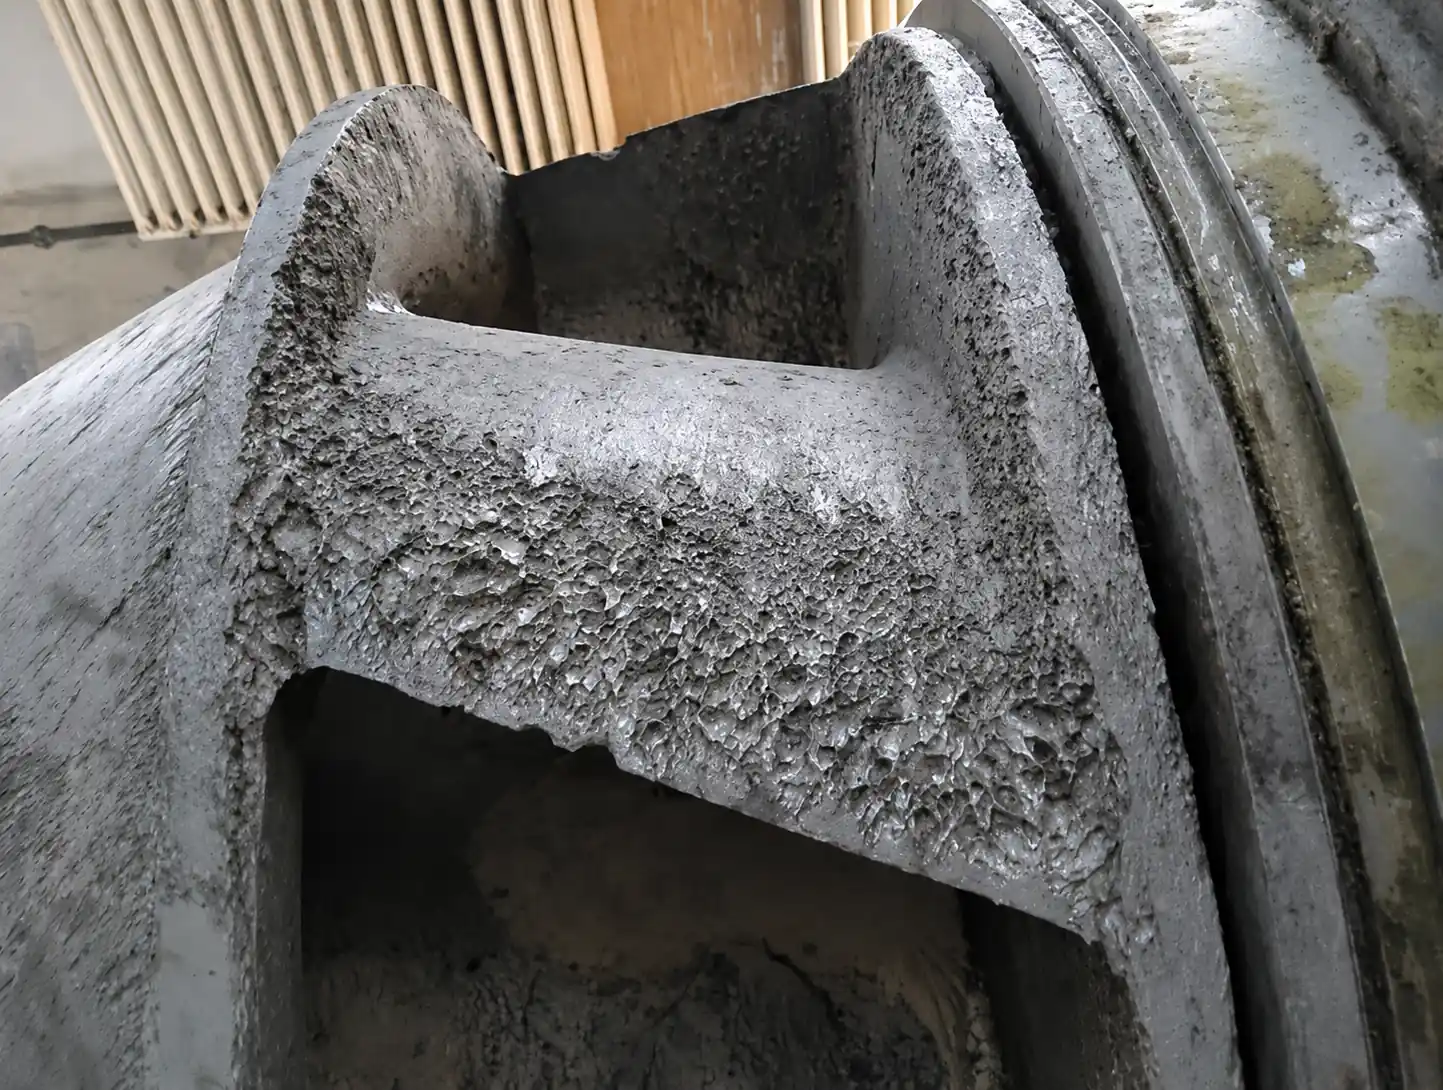
Flashing, cavitation and erosion are different failure mechanisms
Flashing keeps vapour in the downstream flow
Liquid accelerates as it passes through the throttling area. Static pressure reaches its minimum near the vena contracta, which is the narrowest effective flow area just downstream of the restriction. If this local pressure falls below vapour pressure, part of the liquid changes into vapour.
Flashing occurs when the outlet pressure, P2, also remains below vapour pressure. The bubbles do not return to liquid. The valve outlet and downstream pipe carry a high-velocity liquid-vapour mixture that can produce smooth, washed surfaces and directional metal loss. Noise and vibration may be lower than in severe cavitation, but the sustained two-phase velocity can still damage trim and piping.
Cavitation completes a formation-and-collapse cycle
Cavitation starts with the same local vaporisation. It becomes destructive when downstream pressure recovers above vapour pressure. The bubbles then collapse and produce microjets, shock waves, and short local temperature rises close to a metal surface.
Collapse pressures are often described as reaching thousands of atmospheres at a microscopic point. This is a short local event, not a pipeline design pressure. Repeated impacts remove the protective surface film, work-harden the metal, start pits, and turn small defects into a rough honeycomb or cinder-like surface.
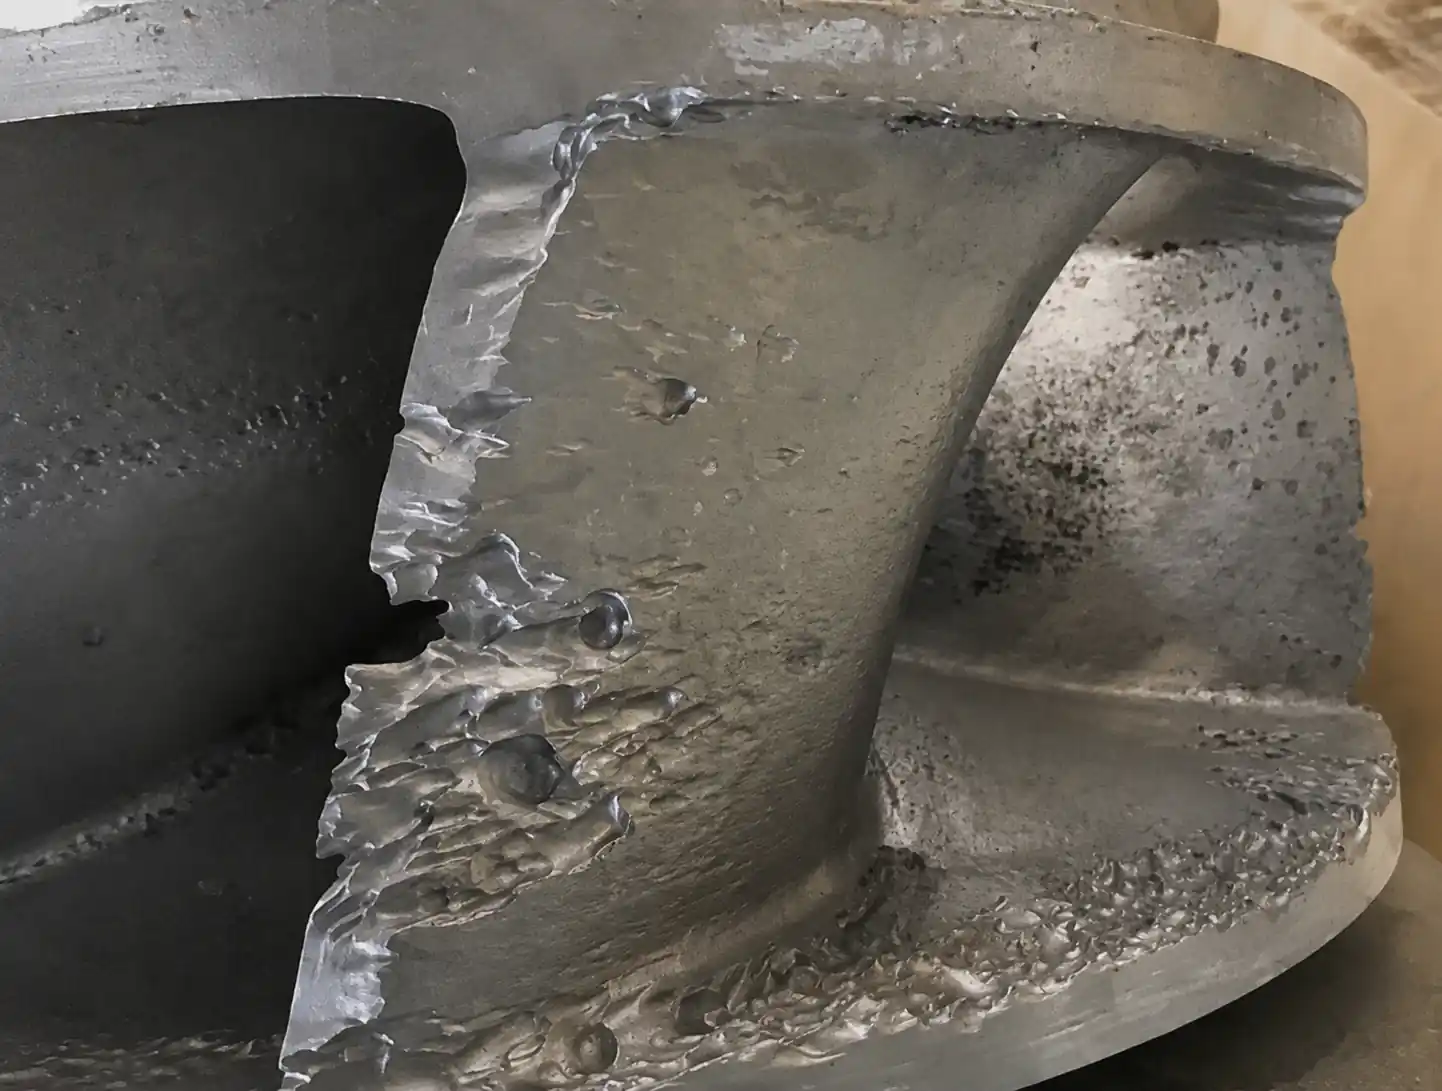
Erosion cuts the surface in the flow direction
Erosion comes from mechanical impact and shear. It becomes more severe when the liquid contains catalyst fines, coal particles, ash, sand, scale, or other solids. The wear often follows the jet direction and leaves grooves, scratches, or a locally thinned edge.
High shear can also remove a corrosion film and expose fresh metal. Corrosion then weakens the surface while erosion removes the new corrosion products. This erosion-corrosion cycle can progress faster than either mechanism alone.
| Feature | Flashing | Cavitation | Erosion |
|---|---|---|---|
| Main trigger | P2 stays below vapour pressure | Pressure recovers above vapour pressure | Velocity, solids, or an impinging jet |
| Vapour behaviour | Bubbles remain in the flow | Bubbles collapse downstream | Bubble formation is not required |
| Typical surface | Smooth, washed, or polished metal loss | Pits, honeycomb texture, or rough craters | Directional grooves, scratches, or edge thinning |
| Common field clue | Steady two-phase noise with less crackling | Sharp crackling, vibration, or a gravel-like sound | Wear aligned with the flow or particle path |
| First control priority | Manage two-phase velocity and outlet geometry | Change the pressure profile or collapse location | Reduce jet velocity and improve wear resistance |
A quick field rule is useful: sharp noise with honeycomb pitting suggests cavitation; smoother washed wear suggests flashing; directional grooves suggest erosion. The rule narrows the inspection, but pressure and process data must confirm the cause.
Pressure recovery decides whether vapour collapses or remains
The pressure drop shown on a line gauge is not the lowest pressure inside a control valve. Local velocity peaks near the vena contracta, so the minimum internal pressure can be below vapour pressure even when the measured outlet pressure is higher.
The pressure path can be read with four values:
- P1: valve inlet pressure before throttling.
- Pvc: minimum pressure at or near the vena contracta.
- Pv: liquid vapour pressure at the actual flowing temperature.
- P2: recovered pressure at the valve outlet.
Vapour begins to form when Pvc falls below Pv. If P2 rises above Pv, cavitation becomes possible. If P2 remains below Pv, the flow continues to flash downstream.
Severe flashing or cavitation may also lead to liquid choked flow. Once the valve reaches the choking limit, a further reduction in downstream pressure does not produce the expected increase in liquid flow. Choking describes a capacity limit; it does not by itself predict the rate of trim damage. The distinction is explained further in the control valve choked-flow guide.
Damage often extends beyond the plug and seat
The highest-risk location is where low static pressure, pressure recovery, a high-velocity jet, and a change in flow direction meet. That point may be inside the trim, but it may also be in the first downstream fitting.
Inspection should cover these peer locations:
- Trim outlet: check the downstream side of the plug, seat ring, cage, and throttling passages.
- Reducer small end: check the area where the cross-section changes and local velocity rises.
- First elbow: inspect the outer wall where a two-phase or particle-laden jet changes direction.
- Downstream pipe: compare wall thickness around welds, fittings, and known impingement zones.
Diagnose the failure mode before changing the trim
A repeatable diagnosis follows the pressure path and the damage path in the same order:
- Map the damage: record whether metal loss starts at the restriction, recovery zone, reducer, elbow, or pipe wall.
- Classify the surface: separate pitting, smooth washing, directional grooves, corrosion products, and impact marks.
- Check the liquid state: use vapour pressure at the actual temperature, not a room-temperature value.
- Compare operating cases: review minimum, normal, and maximum flow with their real P1 and P2 values.
- Review installed travel: compare valve opening, flow demand, and pressure drop rather than judging valve size from line size.
- Confirm the material condition: check coating loss, hardness, weld-overlay condition, and corrosion beneath the worn area.
Sharp crackling and strong vibration support a cavitation diagnosis, but noise alone is not proof. A flashing jet can also be noisy, solids can produce impact noise, and loose parts can create vibration without either phase-change mechanism.
Valve travel gives another clue. A normal operating range of about 40% to 70% travel is a useful sizing rule of thumb for many applications. Long operation below 20% often points to an oversized valve, a narrow high-velocity throttling area, or poor installed control. These percentages are not universal cavitation limits; the installed flow characteristic and the actual pressure cases still govern. The control valve sizing guide explains why Cv, travel, and pressure drop must be reviewed together.
Control pressure and velocity before relying on harder materials
A practical maintenance rule gives selection and pressure-distribution changes about 80% of the preventive work, with material hardening acting as the second line of defence. This 80/20 split is a priority rule, not a measured guarantee. Harder trim may last longer, but it cannot stop vapour formation caused by the wrong pressure profile.
Reduce cavitation by dividing or relocating the pressure drop
Cavitation control aims to keep the minimum internal pressure above vapour pressure or to keep bubble collapse away from vulnerable metal. Suitable measures depend on the required Cv, rangeability, fluid cleanliness, and available downstream pressure.
- Use staged pressure reduction: labyrinth, multi-hole, or stacked-disc trim divides one large pressure drop into several smaller drops.
- Consider angle or Y-pattern flow paths: the geometry can reduce direct impingement and move the outlet jet away from critical surfaces.
- Split the duty between valves: series control stages can reduce the pressure drop carried by one throttling element.
- Raise effective backpressure carefully: a downstream restriction may reduce valve pressure drop when the full system is recalculated.
- Keep useful operating travel: avoid a valve that spends most of its duty below 20% opening when a better Cv selection is possible.
Multi-stage trim should be sized so that each stage limits local pressure and velocity. Some low-noise multi-stage designs report reductions of 15 to 20 dBA, but the result depends on the baseline valve, stage design, flow rate, pressure ratio, piping, and test method. It should not be written as a guaranteed reduction for every application.
A downstream orifice is not an automatic cure. If it raises P2 only enough to make vapour collapse downstream while Pvc remains below Pv, it can turn sustained flashing into cavitation or move the collapse zone. The system must be calculated so that the changed pressure distribution actually removes the harmful condition.
Manage flashing as a sustained two-phase flow
When the required downstream pressure is below vapour pressure, the final part of the pressure drop cannot be designed away inside the valve. The task changes from preventing collapse to controlling velocity, jet direction, and the surfaces exposed to the liquid-vapour mixture.
- Use an angle-body outlet where suitable: the flow path can reduce a direct turn and provide a larger downstream connection.
- Increase outlet flow area: a larger valve outlet or downstream pipe lowers two-phase velocity after flashing begins.
- Protect the downstream path: apply wear-resistant material where the jet contacts the body, reducer, elbow, or pipe wall.
- Avoid abrupt transitions: a longer reducer spreads the area change and can lower local shear and impingement.
- Control solids separately: particle loading adds erosion even when the flashing pressure profile cannot be changed.
Standard ball and butterfly valves are high-recovery designs in many throttling arrangements, so they need careful review for severe cavitating liquid service. This is not a blanket ban on rotary valves. Special trim, reduced-port geometry, staged elements, or a different system pressure profile may change the result.
Surface hardening improves resistance, not the pressure profile
Hardness, layer thickness, bond type, toughness, and corrosion resistance all affect service life. HRC and HV values use different hardness scales and should not be compared as if they were the same number. The values below reproduce the supplied process data and should be confirmed against the selected alloy, substrate, coating procedure, test method, and service temperature.
| Treatment | Layer thickness | Surface hardness | Features and suitable use |
|---|---|---|---|
| Stellite hardfacing | 2 to 5 mm | 38 to 44 HRC | Thick metallurgical bond; reported for temperatures above 800°C; used on high-temperature, high-pressure sealing surfaces |
| Solid cemented carbide | Solid component | Up to 70 HRC or higher | Very hard; suited to small, high-pressure-drop trim where brittleness and joining can be controlled |
| Nitriding | Less than 300 µm | Less than 1200 HV | Low distortion; useful for stainless steel stems; selected processes can balance wear and corrosion resistance |
| Hard chrome plating | 20 to 50 µm | Less than 1200 HV | Low cost and low distortion; thin layer can crack or peel under severe pressure-drop and impact duty |
| PVD coating | 1 to 5 µm | Up to 2000 HV or higher | Very hard with low friction; one precision ball-valve test reported 2.5 times the life of sprayed WC |
| HVOF coating | 0.1 to 0.5 mm | Up to 74 HRC | Physical bond; used for coal slurry and grey-water solids; source data flags delamination risk above Class 1500 |
| Nickel-base spray and fuse | 0.5 to 1.0 mm | 55 to 64 HRC | Metallurgical bond with wear and corrosion resistance; used for grey water, black water, and slag service |
| Laser cladding | More than 1.5 mm | Up to 1162 HV | Metallurgical bond and low dilution; suited to areas needing a thick, hard wear layer |
The table is a screening reference, not a substitute for a qualified coating or welding procedure. The PVD 2.5-times result comes from a specific test, and the HVOF Class 1500 warning is a source-specific risk flag. Pressure class alone does not prove that a coating will fail.
Material selection should account for the following independent checks:
- Bond type: metallurgical bonds usually tolerate impact differently from mechanically bonded coatings.
- Layer thickness: a thin hard film may resist sliding wear but offer little repair allowance.
- Toughness: very high hardness can increase cracking or brittle-fracture risk.
- Corrosion: coating pores, cracks, and exposed edges can allow under-film attack.
- Temperature: substrate strength and coating stability may fall before the quoted hardness limit.
- Geometry: small passages, sharp edges, and sealing surfaces have different finishing and tolerance needs.
Two reported cases show why the remedy must match the mechanism
Drain-pipe reducer damage
The drain-pipe case placed the severe damage at the reducer rather than only inside the valve. The CFD result linked low static pressure, vaporisation, and a 582.1 Pa peak wall shear stress in the same local region. A longer reducer was recommended because a slower area change can lower acceleration and wall shear. The reported 150 mm to 400 mm modification should not be copied without checking flow rate, diameter ratio, pressure recovery, and available layout space.
Boiler blowdown angle-valve retrofit
The supplied industry report describes a boiler blowdown angle valve reducing pressure from 19.73 MPa to 1.03 MPa. Severe cavitation damaged the original trim. The retrofit added a multi-stage anti-cavitation cage so that energy was released through several restrictions rather than one large pressure drop.
- Reported pressure duty: 19.73 MPa inlet to 1.03 MPa outlet.
- Reported modification: a multi-stage pressure-reducing anti-cavitation cage.
- Reported service result: life extended by at least one year.
- Reported cost result: RMB 300,000 to 400,000 saved per year in replacement costs.
These figures are useful as a reported application example, but the original project report was not available for independent review. They should not be treated as a guaranteed result for another boiler, pressure ratio, valve size, or duty cycle.
Inspection should follow the expected damage path
Operating checks can detect a change before the next shutdown:
- Listen for change: record new crackling, rising broadband noise, or a shift in vibration.
- Trend valve travel: note long operation below 20%, unstable travel, or a new operating position for the same flow.
- Track pipe thickness: measure the first reducer, elbow, weld area, and known jet-impact zone.
- Watch capacity: compare commanded travel with actual flow for signs of choking, blockage, or trim damage.
During shutdown, inspect the plug, seat, cage, body outlet, reducer, and first elbow as one flow path. Photograph the surface before cleaning, then record the location and direction of pits, grooves, smooth washing, coating loss, and corrosion products. For labyrinth or multi-hole trim, check small passages for solids and deposits because a design that controls cavitation in clean liquid may plug in slurry service.
Conclusion
Flashing calls for control of sustained two-phase velocity. Cavitation calls for a different pressure-recovery path. Particle erosion calls for velocity control, jet management, and wear-resistant materials. The correct order is to identify the mechanism, change the pressure or flow path where possible, and then select a surface treatment for the remaining exposure. For severe pressure-drop duties, compare the available approaches in the control valve trim guide for cavitation and noise.